
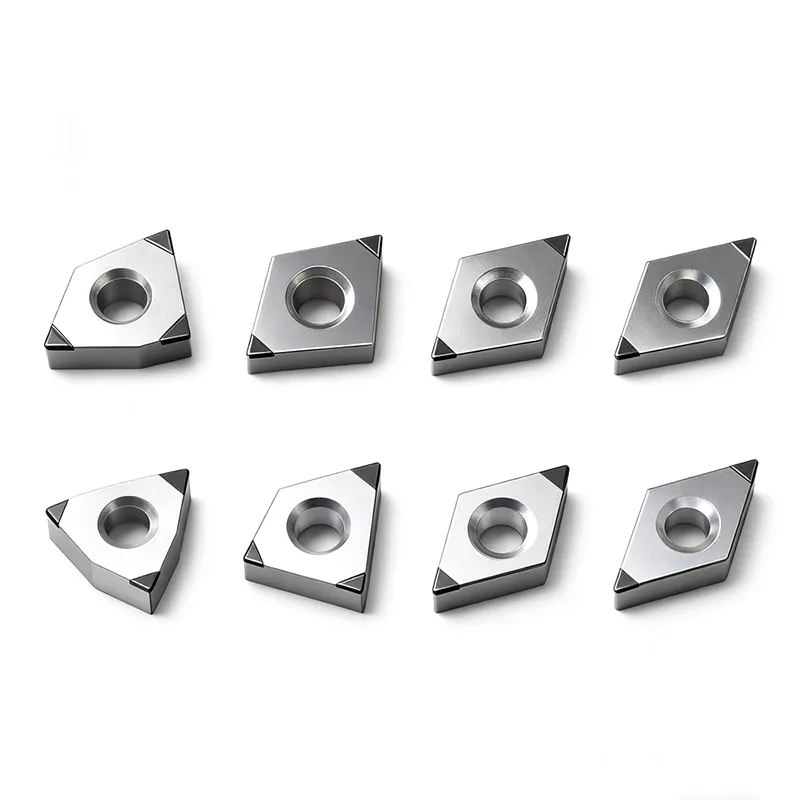
Ceramic-coated CBN Insert
In the demanding world of precision machining, achieving superior surface finishes and extended tool life on hardened steels and difficult-to-cut alloys is a constant pursuit. Our advanced Ceramic-coated CBN Insert is engineered to be the definitive solution, offering a unique combination of extreme hardness, thermal stability, and wear resistance. This innovative tool is specifically designed to excel in high-speed, high-temperature finishing operations. For applications requiring the ultimate in material integrity, our High-hardness CBN Insert provides unmatched resistance to abrasive wear. When dimensional accuracy is non-negotiable, the High-precision CBN Insert ensures consistent, tight-tolerance machining. The inherent High-temperature Resistant CBN Insert properties are further enhanced by our proprietary ceramic coating, allowing it to maintain cutting edge integrity under intense thermal loads. For interrupted cuts or unstable conditions, the robust design of our Impact-resistant CBN Insert offers exceptional durability and reliability.
The exceptional performance of the Ceramic-coated CBN Insert stems from its meticulously engineered multi-layer architecture. At its core is a premium Cubic Boron Nitride (CBN) substrate, selected for its extreme hardness second only to diamond. This substrate is then bonded to a rugged tungsten carbide base, providing excellent shock absorption and structural support. The critical innovation is the application of a state-of-the-art ceramic coating via a controlled PVD (Physical Vapor Deposition) process. This ultra-thin, yet incredibly tough coating acts as a thermal barrier, significantly reducing heat transfer to the substrate and minimizing chemical diffusion and oxidation at the cutting edge. The result is a tool that maintains a sharper cutting edge for longer, dramatically reducing friction, built-up edge formation, and overall tool wear. This directly translates to higher machining speeds, improved part quality with exceptional surface finishes, and a substantial increase in productivity by reducing downtime for tool changes.
Key Specifications & Technical Data
- Substrate Material: High-density CBN content (60% - 65%) on Tungsten Carbide base
- Coating Type: Multi-layered PVD Ceramic Coating (AlTiN/TiSiN based)
- Coating Thickness: 3 ~ 5 microns
- Hardness (HV): Substrate: >3500; Coating Surface: >3200
- Thermal Stability: Stable up to 1200°C (2192°F)
- Primary Application: Finish machining of hardened steels (45-65 HRC), gray cast iron, and powder metals
- Recommended Cutting Speed (Vc): 200 - 450 m/min for hardened steel
| Grade Code | CBN Content | Binder Phase | Best For Material Hardness (HRC) | Nose Radius (Typical) |
|---|---|---|---|---|
| CCBN-H10 | 60% | TiC/TiN | 50 - 58 | 0.4 mm, 0.8 mm |
| CCBN-H20 | 65% | TiAlN | 55 - 62 | 0.2 mm, 0.4 mm |
| CCBN-H30 | 60% | Ceramic Enhanced | 45 - 55 (High-speed finishing) | 0.8 mm, 1.2 mm |
Performance Advantages & Comparison
| Performance Metric | Standard CBN Insert | Ceramic-coated CBN Insert | Improvement |
|---|---|---|---|
| Tool Life in Hard Steel Machining | Base Reference | 2X - 4X Longer | +200% to +300% |
| Average Surface Finish (Ra) | 0.4 - 0.6 μm | 0.2 - 0.3 μm | Up to 50% Smoother |
| Maximum Sustainable Cutting Speed | ~300 m/min | ~450 m/min | +50% Higher Speed |
| Resistance to Thermal Cracking | Moderate | Excellent | Significantly Enhanced |
Related Products


Hot Products
Drilling and Threading Cutters for Machining ISO-metric Threads
Searching for a reliable China Manufacturer of high-performance Drilling and Threading Cutters for Machining ISO-metric Threads? At Wangdefu, we specialize in ISO-standard threading solutions for automotive, aerospace, mold, and precision machinery applications. Our cutters combine drilling, chamfering, and thread milling in one tool, achieving IT6–IT7 thread accuracy, Ra0.8μm surface finish, and enhanced efficiency compared to traditional “drill + tap” methods. Trust Wangdefu for long-lasting, high-precision tooling that reduces scrap and boosts productivity.
Carbide Flathead Drill
Wangdefu, a professional China Manufacturer and Supplier, has been focusing on high-precision CNC tools and parts processing for more than ten years. Our Carbide Flathead Drill excels in automotive, robotics, aerospace and mold manufacturing.
PCD Non Standard Reamers
WDF specializes in PCD Non Standard Reamers, providing design, production, and customization as a reliable China factory and supplier. With extensive experience in ultra-hard tooling, we serve the automotive, 3C (mobile phone and computer), and aerospace industries. Our reamers tackle high-precision holemaking for aluminum, copper, and composite parts, helping customers improve efficiency, accuracy, and overall product quality.
Solid Carbide Drills
Solid Carbide Drills from WDF are crafted from premium materials for precision hole forming. As a professional China manufacturer and supplier with factory-level production, our drills offer precise, one-pass cutting that eliminates repeated drilling, saving time and improving efficiency. Durable and abrasion-resistant, they perform reliably in high-speed machining of steel, alloys, and other challenging materials. Trusted by automotive, machine shop, and electronics industries, WDF delivers high-performance, efficient, and stable drilling solutions.
Cast Iron Precision Face Milling Cutter
Wandefu is a manufacturer with many years of experience in the production of Cast Iron Precision Face Milling Cutter. With years of solid research and accumulation, we have long been a trusted benchmark in the industry.Mature production technology and advanced technology and equipment, so that each Wandefu cast iron finish milling cutter has undergone layers of strict quality control, from raw material selection to finished product testing, no details are omitted, in order to ensure the high precision performance of the product.It is this dedication to quality that makes our products outstanding in the field of automotive parts manufacturing.Choosing Wandefu means choosing precision, quality and confidence.
PCD Inserts
WDF is a professional China supplier specializing in PCD inserts. With many years of experience in the super-hard tooling industry, we have set an industry benchmark through advanced research and a precise understanding of customer needs. As a reliable manufacturer and factory-level provider, WDF has become a trusted partner for companies worldwide, delivering high-quality, precise, and durable cutting solutions.
- Related Blog
- Reviews

