
Impact-resistant CBN Insert
Unmatched Durability for Demanding Machining: The Impact-resistant CBN Insert
In the relentless world of machining hardened steels, cast irons, and superalloys, tool failure due to sudden shocks and interrupted cuts is a constant, costly challenge. Standard tools chip and wear prematurely, leading to downtime, scrap, and lost productivity. This is where the engineering superiority of our High-hardness CBN Insert is fully leveraged. We've engineered a cutting tool specifically to withstand these punishing conditions. By combining extreme hardness with a specialized bonding system and robust geometry, this insert delivers exceptional fracture resistance without sacrificing cutting performance. It is the definitive solution for applications involving milling, rough turning, and operations with variable depths of cut where impact is inevitable. Whether you are machining complex automotive components, heavy industrial castings, or aerospace forgings, this insert maintains its cutting edge integrity far longer than conventional options.
The core advantage of this insert lies in its tailored composition. Unlike standard CBN grades that prioritize pure wear resistance, this grade is optimized for toughness. The carefully selected CBN grain size and a dedicated metallic-ceramic binder work in unison to absorb and dissipate the energy from impacts, preventing catastrophic failure. This makes it exceptionally reliable for CBN Insert for Ferrous Metals in unstable environments. Furthermore, its inherent stability ensures consistent High-precision CBN Insert results even after sustaining minor shocks, protecting your part tolerances. The substrate and edge preparation are also critical, providing unparalleled support to the cutting edge. When paired with its excellent High-temperature Resistant CBN Insert properties, it allows for secure use at elevated speeds and feeds, pushing productivity boundaries while maintaining tool security.
Engineered Specifications of the Impact-resistant CBN Insert
The performance of the Impact-resistant CBN Insert is defined by its precise and robust specifications. This insert is not a generic tool; it is a purpose-built solution for high-impact machining. Below are the key parameters and technical data that underscore its professional-grade design and capability.
Core Material Properties & Geometry
- Primary Composition: High-density Cubic Boron Nitride (CBN) grains within a toughened ceramic-metallic binder matrix.
- Key Feature: Engineered for optimal micro-fracture resistance and thermal shock endurance.
- Standard Coating: A specialized multilayer PVD coating (e.g., TiAlN/AlCrN) is applied to enhance lubricity and further resist abrasive wear and cratering.
- Edge Preparation: Features a reinforced T-land (chamfer) edge hone. The specific combination of land width and hone radius is critical for absorbing impact forces while protecting the cutting edge.
- Grade Designation: IC (Impact-resistant CBN) series, with sub-grades available for varying workpiece material groups.
Technical Specifications & Application Data
| Parameter | Specification / Range | Notes |
|---|---|---|
| CBN Content | 50% - 65% by volume | Balanced for toughness and wear resistance. |
| Grain Size | 3 - 8 micrometers | Medium-coarse grains for superior fracture resistance. |
| Hardness (HV) | 3,200 - 3,500 HV | Extremely high hardness retained at operating temperatures. |
| Transverse Rupture Strength (TRS) | > 1,500 MPa | Quantifies exceptional resistance to breaking under bending stress. |
| Thermal Stability | Up to 1,200°C (2,192°F) | Maintains chemical integrity and hardness in high-heat zones. |
| Recommended Workpiece Materials | Hardened steel (45-65 HRC), Gray & Ductile Cast Iron, Hardfacing alloys, Nickel-based superalloys. | Ideal for interrupted cuts on these materials. |
| Starting Cutting Speed (Vc) | 80 - 180 m/min (260 - 590 SFM) | Varies based on material and operation; consult technical guide. |
| Feed per Revolution (f) | 0.10 - 0.30 mm/rev (0.004 - 0.012 IPR) | Robust geometry supports higher feeds in roughing. |
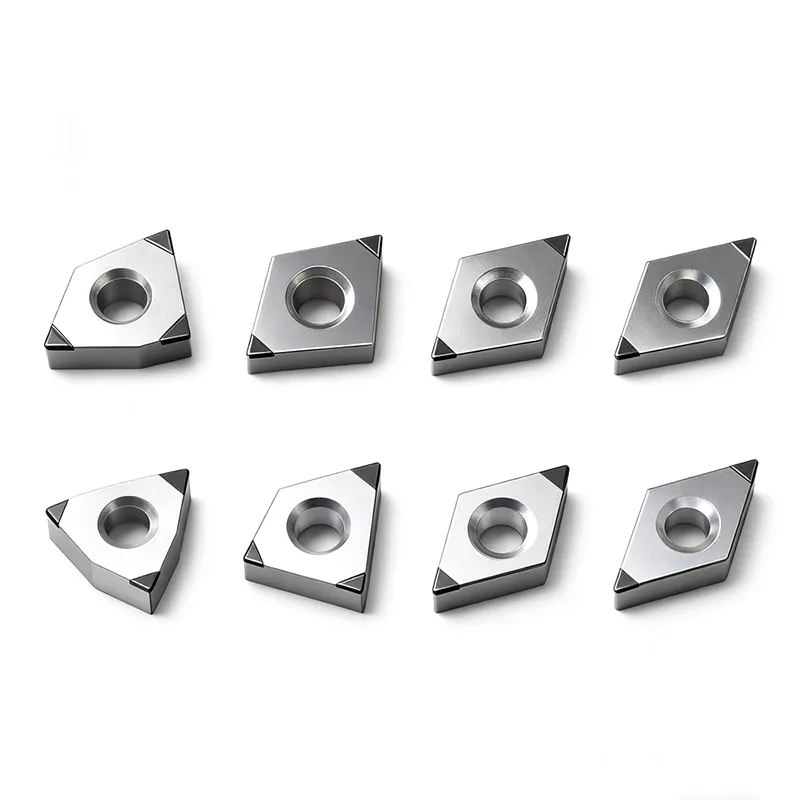
| Standard Styles | CNGA, DNGA, SNMA, RCMT, etc. | Available in common negative and positive rake styles with chipbreakers. |
| Primary Applications | Interrupted turning, milling, roughing, facing of castings/forgings. | Where shock loading is a primary concern. |
Related Products


Hot Products

Carbide Twist Drill Bits
WDF specializes in drilling tools. Our Carbide Twist Drill Bits are made from top-quality, hardened carbide! They're incredibly tough, incredibly durable, and incredibly durable, making them perfect for high-speed cutting. They produce precise, smooth holes, work incredibly quickly, and eliminate the need for subsequent repairs. Their unique design makes them easy to drill even high-hardness metals and difficult-to-cut materials. They're used in industries like machine tools, automotive parts, and aerospace—the perfect choice for demanding work!
Thread Cutting Taps
Wanderfu specializes in the research, development, and production of thread cutting taps and has many years of industry experience. As a trusted China manufacturer and supplier, we offer a comprehensive range of taps and are recognized globally for consistent quality. Our professional engineering team continuously optimizes various styles, including straight flute, spiral flute, and spiral point taps, ensuring reliable performance for every machining application. With factory-level capabilities, Wanderfu delivers efficient and precise solutions to meet customer demands worldwide.
Straight Flute Reamer
Straight Flute Reamers from WDF are produced by a leading China manufacturer specializing in CNC tooling. With years of experience, our factory-level capabilities and professional team ensure innovative technology and superior quality. As a trusted supplier, WDF continuously improves tool precision and performance, delivering high-quality solutions and excellent service to meet diverse customer needs.
Aerospace CNC Prototype Machining
As a trusted China manufacturer and supplier, Wangdefu specializes in Aerospace CNC Prototype Machining, providing high-precision custom machining services for aerospace engine components, spacecraft structural parts, and onboard equipment assemblies. Leveraging advanced five-axis CNC machining centers and ultra-precise inspection equipment, we handle challenging materials such as titanium alloys, high-temperature alloys, and carbon fiber composites. Our prototypes achieve dimensional tolerances of ±0.003mm and geometric tolerances ≤0.005mm, fully meeting the stringent quality and performance requirements of the aerospace sector.
CNC Tapping Tool Handle
Looking for a reliable CNC tapping tool handle from a professional China manufacturer and supplier? Wangdefu provides high-precision CNC tapping tool systems that integrate threading tap holders, floating collets, and torque overload protection for safe, accurate, and efficient threading. Designed for automotive, mold-making, 3C electronics, and precision machinery industries, our solutions reduce tap breakage, improve thread quality, and enhance production efficiency. As a trusted factory and brand, Wangdefu ensures you get the best results with every project.
Right-Angle Plane Milling Cutter
Our Right-Angle Plane Milling Cutter is a high-performance tool designed for high-precision milling, face machining, and planar cutting. It is widely used in automotive parts, new energy motor housings, aerospace components, and robot structural parts.
As a professional manufacturer in China, Wangdefu not only provides cutting tools but also complete machining solutions, from tool selection and parameter recommendations to installation guidance and after-sales service, helping customers achieve high-efficiency, high-precision, and low-cost machining.
- Related Blog
- Reviews

