
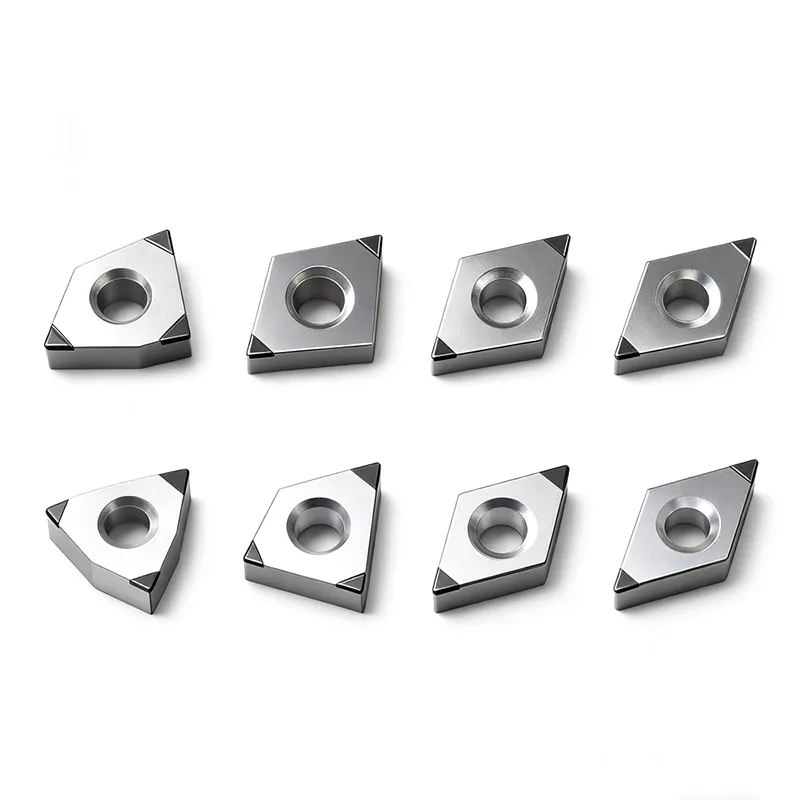
High-temperature Resistant CBN Insert
In the demanding world of precision machining, where ferrous alloys push tools to their limits, thermal stability is not merely an advantage—it's a requirement for success. Our High-temperature Resistant CBN Insert is engineered specifically to excel in these extreme environments, maintaining its cutting edge integrity where conventional tools fail. This insert is the cornerstone for machining hardened steels, cast irons, and superalloys, delivering unparalleled performance and extended tool life. For applications demanding ultimate material integrity, our High-hardness CBN Insert provides the necessary durability. When micron-level accuracy is non-negotiable, the High-precision CBN Insert ensures flawless finishes. In operations prone to intermittent cuts or vibration, an Impact-resistant CBN Insert is essential for reliability. Ultimately, for all ferrous metal machining challenges, our comprehensive CBN Insert for Ferrous Metals lineup offers a specialized solution.
The core innovation of the High-temperature Resistant CBN Insert lies in its advanced composition and robust design. It utilizes a premium cubic boron nitride (CBN) content, strategically bonded with a ceramic phase that provides exceptional thermal and chemical stability. This unique structure allows the insert to withstand continuous cutting temperatures exceeding 1200°C without significant wear or deformation. The substrate is crafted from a specially formulated tungsten carbide, offering superior support and heat dissipation to protect the CBN layer. A proprietary post-treatment process further enhances the edge strength and surface quality, ensuring consistent performance from the first cut to the last. This makes the High-temperature Resistant CBN Insert an indispensable tool for high-speed dry machining, hard turning, and milling applications where heat is the primary adversary.
Key Specifications & Technical Data
- Primary Application: Hard turning, finishing, and high-speed machining of ferrous metals (HRC 45-68).
- CBN Grade: High-density, fine-grained CBN with high thermal stability.
- Bonding System: Ceramic-based binder for enhanced heat and wear resistance.
- Substrate Material: Tough tungsten carbide with high thermal conductivity.
- Coating: Optional proprietary TiAlN multilayer coating for abrasive applications.
- Temperature Resistance: Stable performance in continuous cutting up to 1200°C (2192°F).
| Insert Style | CBN Content | Recommended Cutting Speed (m/min) | Feed Rate (mm/rev) | Depth of Cut (mm) | Typical Workpiece Material |
|---|---|---|---|---|---|
| CNGA / RNMN | High (CBN50+) | 80 - 250 | 0.05 - 0.20 | 0.1 - 0.5 | Hardened Steel, Tool Steel |
| SNMA / TNMG | Medium (CBN30) | 100 - 300 | 0.08 - 0.25 | 0.2 - 1.0 | Gray Cast Iron, Chill Cast Iron |
| RCMX / CCGT | High (CBN50+) | 150 - 400 | 0.03 - 0.15 | 0.05 - 0.3 | Powder Metal, Sintered Iron |
For optimal results with the High-temperature Resistant CBN Insert, a rigid machine tool setup with minimal runout is critical. Use positive rake geometries for lower cutting forces and reduced heat generation. A consistent, high-pressure coolant directed at the cutting zone is recommended, though the insert is fully capable of dry machining. Always ensure the workpiece is securely clamped to prevent vibration, which can compromise edge life and surface finish. Implementing these best practices will maximize the productivity gains and cost-effectiveness provided by this advanced cutting tool.
Related Products



Hot Products
Aerospace CNC Prototype Machining
As a trusted China manufacturer and supplier, Wangdefu specializes in Aerospace CNC Prototype Machining, providing high-precision custom machining services for aerospace engine components, spacecraft structural parts, and onboard equipment assemblies. Leveraging advanced five-axis CNC machining centers and ultra-precise inspection equipment, we handle challenging materials such as titanium alloys, high-temperature alloys, and carbon fiber composites. Our prototypes achieve dimensional tolerances of ±0.003mm and geometric tolerances ≤0.005mm, fully meeting the stringent quality and performance requirements of the aerospace sector.
CNC Prototype Model of Stainless Steel Valve Block
CNC Prototype Model of Stainless Steel Valve Block Manifold from China Wangdefu Precision Machinery is crafted with over a decade of CNC machining experience. As a trusted China manufacturer and supplier with factory-level production, we use high-quality stainless steel and precise CNC technology to ensure durability, accuracy, and reliability, meeting the demands of diverse and challenging operating environments.
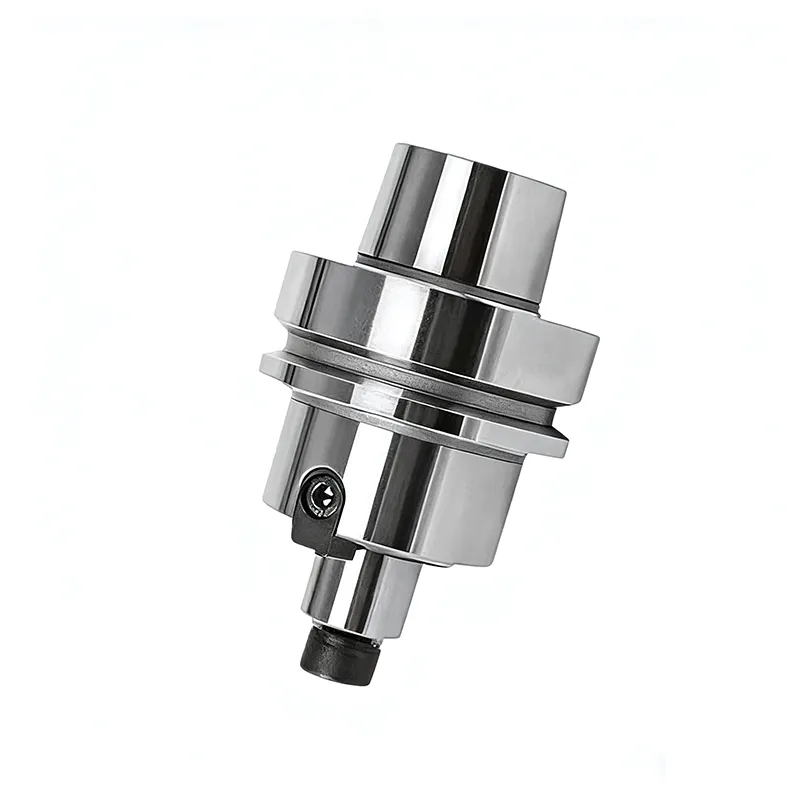
Shrink Fit Chuck
WDF is a high-tech China manufacturer specializing in the research, development, and production of shrink fit chucks. With years of experience in the precision tooling industry, we provide customized solutions focused on high rigidity, low vibration, and quick-change efficiency. Using advanced equipment and factory-level quality control, WDF ensures exceptional performance in high-end manufacturing, earning a strong reputation as a reliable supplier worldwide.
PCD Corn End Mill
PCD Corn End Mills from Wangdefu are not just standard catalogue tools, but mature solutions repeatedly tested and optimized through long-term processing of aluminum alloys, new energy motor shells, and structural parts in our own China factory. As a professional manufacturer and supplier, Wangdefu delivers reliable, high-performance tools for mass production, with real expertise in landing practical machining solutions.
CNC Prototype Humanoid Robot Arm Shell
The CNC Prototype Humanoid Robot Arm Shell produced by WDF, a professional CNC parts manufacturer in China, use high-quality raw materials. Factory direct sales. You can rest assured to choose our products. We guarantee quality and provide thoughtful service for every product to ensure your safe and reliable purchase.
Flat End Mill
WDF specializes in Flat End Mills, with long-term expertise in precision tool manufacturing and application. Ningbo Wangdefu Precision Machinery Co., Ltd. is supported by an experienced technical and service team and implements strict quality control throughout the production process to ensure stable performance and high accuracy. Our milling cutters deliver excellent precision and surface finish, helping automotive parts manufacturers complete complex and high-end machining tasks efficiently. As a reliable China manufacturer, we are committed to building long-term partnerships with global customers.
- Related Blog
- Reviews

