
High-hardness CBN Insert
For demanding machining applications, particularly with hard ferrous materials, achieving optimal results requires cutting tools engineered for extreme performance. Standard carbide inserts often fall short, leading to rapid wear, poor surface finishes, and increased downtime. A High-precision CBN Insert addresses these challenges directly. Crafted from Cubic Boron Nitride, the second hardest material after diamond, these inserts deliver unmatched hardness and wear resistance. Their exceptional stability allows for ultra-tight tolerances and superior surface finishes on hardened steels, cast irons, and other challenging workpieces. To withstand the intense heat generated in high-speed and dry machining operations, a High-temperature Resistant CBN Insert is essential. These grades are specifically formulated with advanced binder systems to maintain their cutting edge integrity and resist thermal cracking at elevated temperatures, ensuring consistent performance and longer tool life. In interrupted cuts or applications involving fluctuating forces, an Impact-resistant CBN Insert provides the necessary toughness. This robustness prevents chipping and micro-fractures, guaranteeing reliable operation in less-than-ideal conditions. When your primary application involves machining hardened steels, bearing steels, or tool steels, a specialized CBN Insert for Ferrous Metals is the definitive solution. These inserts are optimized to handle the unique abrasive and adhesive wear mechanisms presented by ferrous alloys, maximizing productivity and cost-efficiency.
The High-hardness CBN Insert represents a pinnacle of cutting tool technology, designed to transform your machining of hardened materials. Its core advantage lies in a meticulously engineered composite structure. A layer of polycrystalline cubic boron nitride (PCBN) is securely bonded to a tungsten carbide substrate. This combination leverages the extreme hardness of CBN for cutting, supported by the toughness and shock-absorbing properties of the carbide base. The result is a tool that excels in applications where others fail. It enables high-speed machining of components with hardness exceeding 45 HRC, drastically reducing cycle times compared to traditional grinding or using ceramic inserts. Furthermore, the exceptional wear resistance of the High-hardness CBN Insert translates to remarkably consistent part dimensions over extended production runs, minimizing the need for frequent tool changes and recalibrations. This consistency is critical for maintaining tight geometrical tolerances and achieving superior surface integrity on finished parts.
Key Product Parameters & Specifications:
- Material Composition: Polycrystalline Cubic Boron Nitride (PCBN) tip on a Tungsten Carbide substrate.
- Primary Application: Finish machining and hard turning of ferrous metals with hardness > 45 HRC (e.g., hardened steels, tool steels, cast irons).
- Outstanding Properties: Extreme hardness (second only to diamond), excellent thermal stability, and high chemical inertness towards ferrous materials.
- Performance Benefits: Enables high-speed machining, provides exceptional wear resistance leading to long tool life, and produces superior surface finishes.
| Grade Code | CBN Content (%) | Grain Size (µm) | Binder Type | Recommended Cutting Speed (m/min) | Ideal Workpiece Material |
|---|---|---|---|---|---|
| HB10 | 50-60 | 2-4 | Ceramic (TiN/Al2O3) | 100-250 | Hardened Steels (55-65 HRC) |
| HB20 | 80-90 | 4-8 | Metallic (Co, Ni) | 150-350 | Gray Cast Iron, Pearlitic Malleable Iron |
| HB30 | 65-75 | 3-6 | Composite (TiC/TiN) | 80-200 | Interrupted Cuts on Hardened Steels, Powder Metals |
Typical Insert Geometry & Ordering Information:
| ISO Shape Code | Inscribed Circle (IC) Size | Corner Radius (mm) | Clearance Angle | Nose Angle | Standard Coating |
|---|---|---|---|---|---|
| CNGA | 12.7 mm (1/2") | 0.4, 0.8, 1.2 | 7° | 80° | TiAlN |
| DNMA | 15.875 mm (5/8") | 0.8, 1.2 | 0° | 55° | TiCN |
| SNGA | 9.525 mm (3/8") | 0.2, 0.4, 0.8 | 0° | 60° | None / Bare PCBN |
Related Products


Hot Products

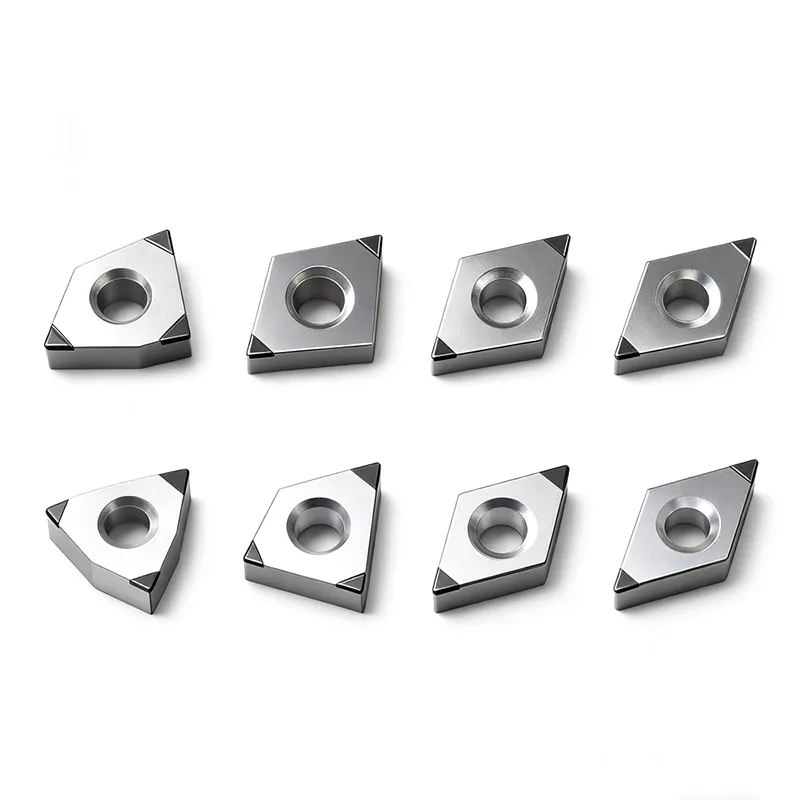
CNC Milling Non-Standard Cutter Head
In the fields of precision machining and high-end manufacturing, efficiency, accuracy, and tool compatibility are the most important concerns for buyers. As a leading supplier in China, Wangdefu focuses on providing high-performance CNC milling non-standard cutter heads to meet the machining needs of various complex parts.
High Speed Steel Twist Drill
High Speed Steel Twist Drills from WDF are premium-quality, cost-effective tools produced by a professional China manufacturer and supplier with factory-level capabilities. With a focus on R&D and meticulous production control—from material selection to finished inspection—our drills deliver reliable performance and excellent value. Trusted by customers worldwide, WDF provides durable, precise, and efficient solutions for various drilling applications.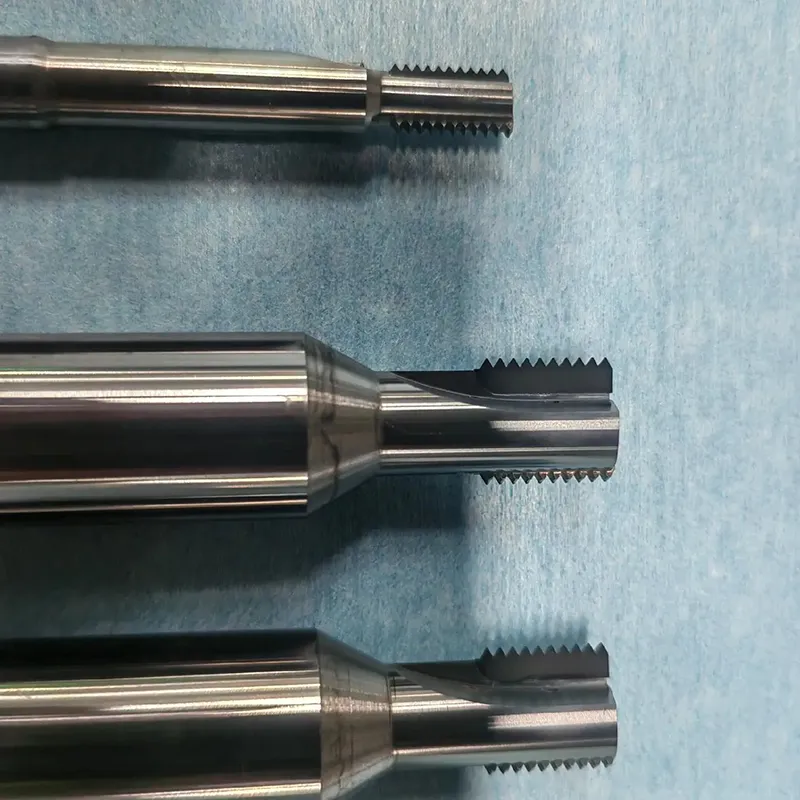
UNF-metric Thread Drilling and Threading Cutter
Looking for a reliable UNF-metric thread drilling and threading cutter manufacturer in China? At Wangdefu, we provide high-precision, long-life UNF cutters suitable for automotive, aerospace, and precision machinery applications. As a trusted supplier and factory, we deliver fast, high-quality solutions to help you reduce production costs and improve efficiency. Our cutters ensure thread accuracy, stable performance, and consistent results across batches, making us your ideal partner for high-precision UNF thread machining.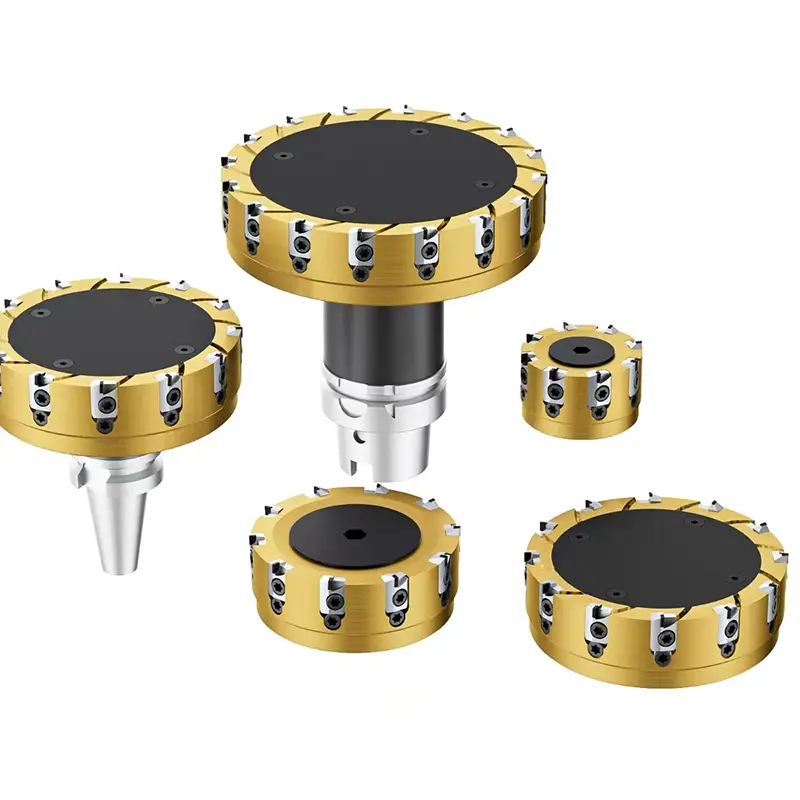
Aluminum Alloy Face Milling Cutter Tool
The Aluminum Alloy Face Milling Cutter Tool from Ningbo Wangdefu Precision Machinery Co., Ltd is designed for high-efficiency, high-precision machining of aluminum and aluminum alloy materials. Backed by years of manufacturing experience and strict factory-level quality control, each cutter delivers stable performance, excellent surface finish, and long tool life for demanding industrial applications.
As a professional China aluminum milling cutter manufacturer and supplier, Wangdefu controls every stage of production—from raw material selection to final inspection—to ensure consistent accuracy and reliable machining results. Our face milling cutters are widely used in automotive parts, aerospace components, and precision mechanical manufacturing.
CNC Prototype Model of Steering Gear Housing
Ningbo Wangdefu Precision Machinery Co., Ltd., with over a decade of experience in CNC machining of automotive parts, proudly launches the high-performance CNC Prototype Model of Steering Gear Housing. Designed specifically for automakers and parts suppliers, this core product embodies our years of experience in precision machining and has successfully served numerous renowned automotive companies.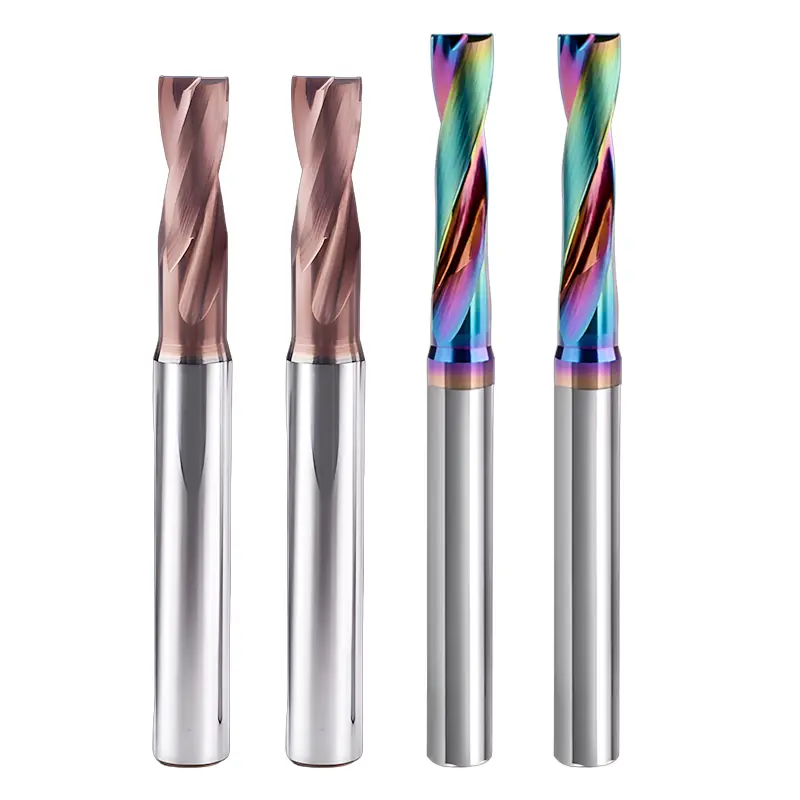
Carbide Flathead Drill
Wangdefu, a professional China Manufacturer and Supplier, has been focusing on high-precision CNC tools and parts processing for more than ten years. Our Carbide Flathead Drill excels in automotive, robotics, aerospace and mold manufacturing.
- Related Blog
- Reviews

