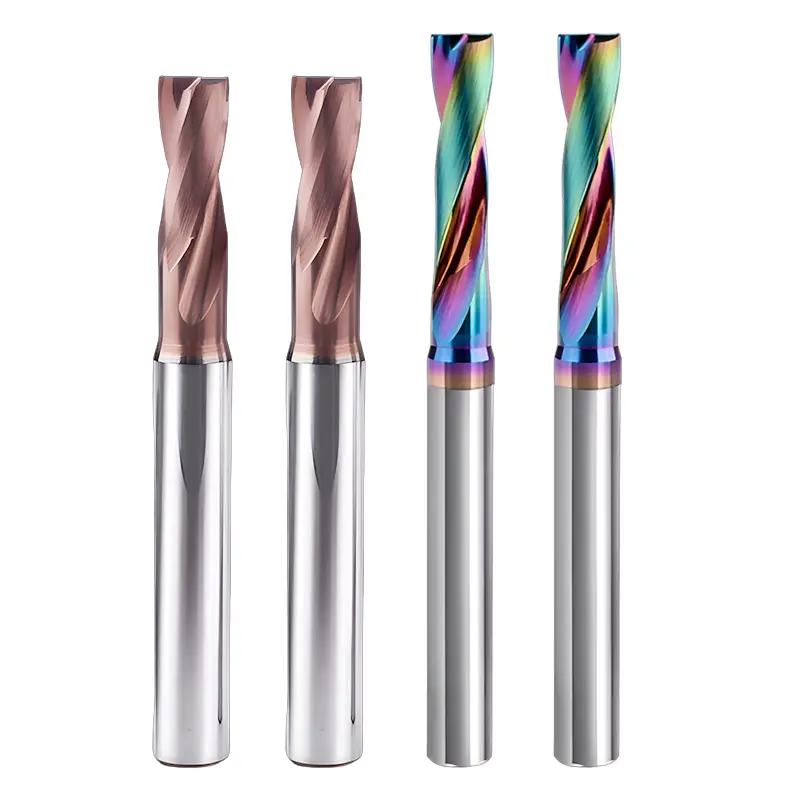
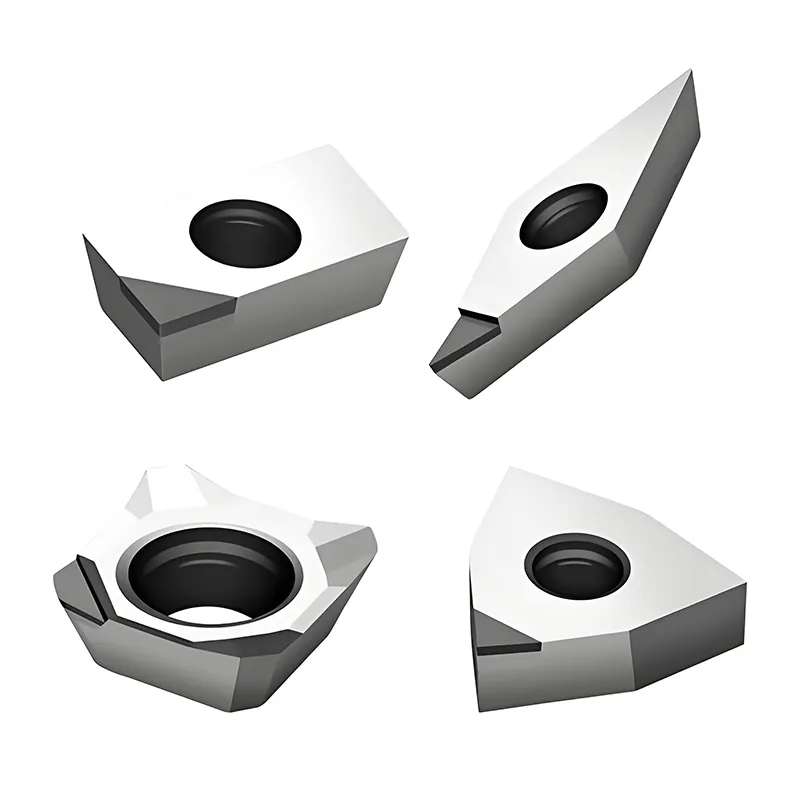
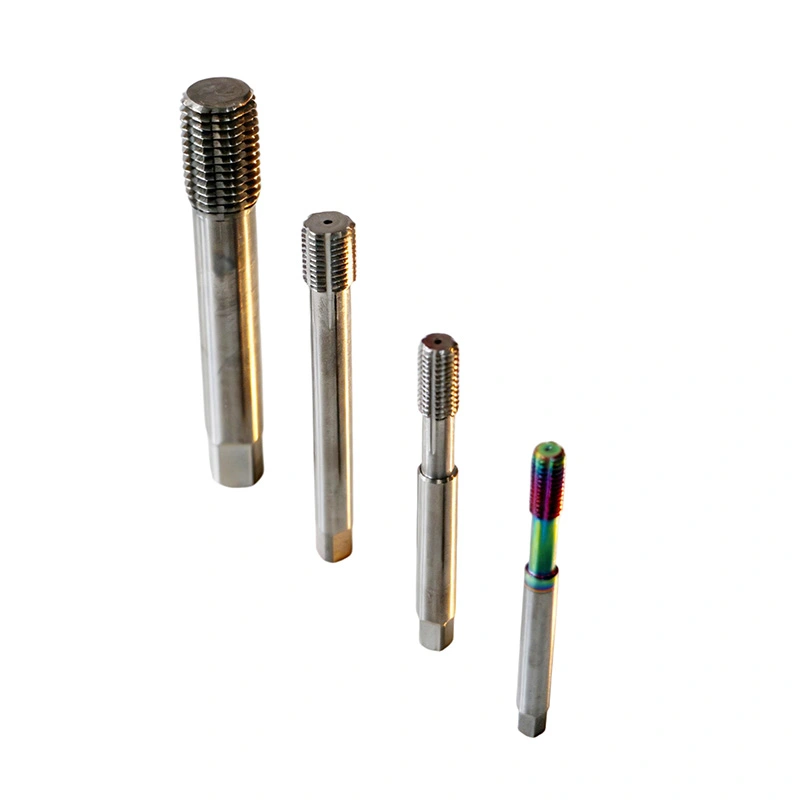
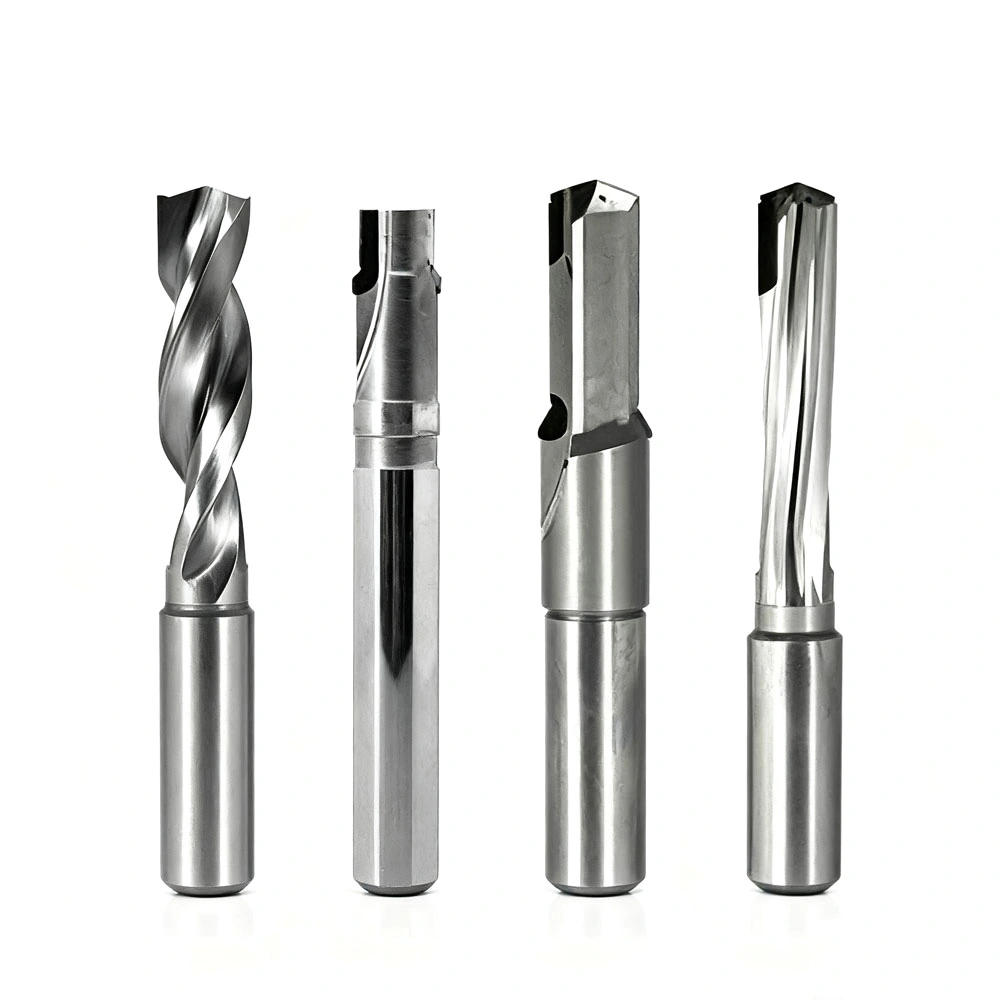
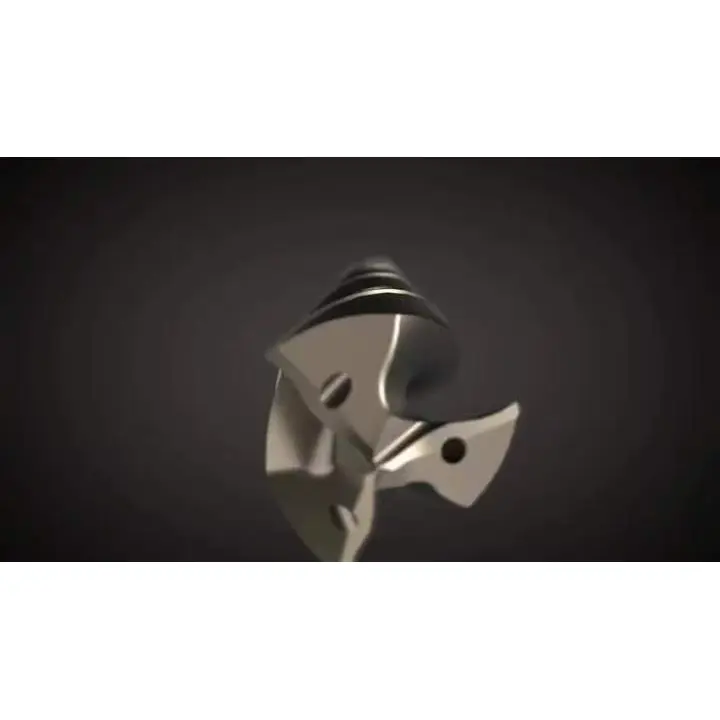
PCD Small Hole Boring Tool
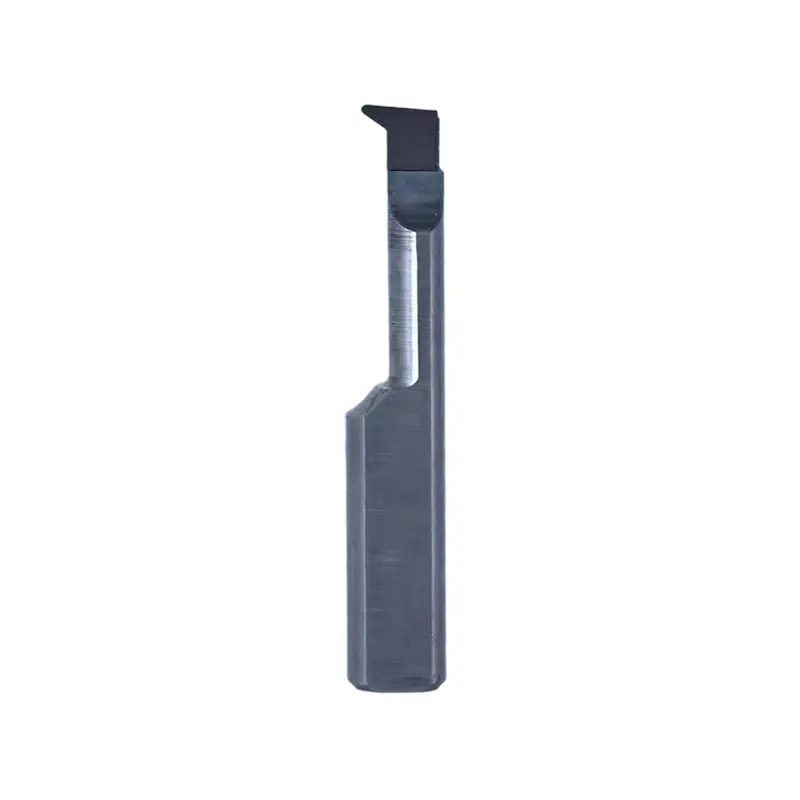
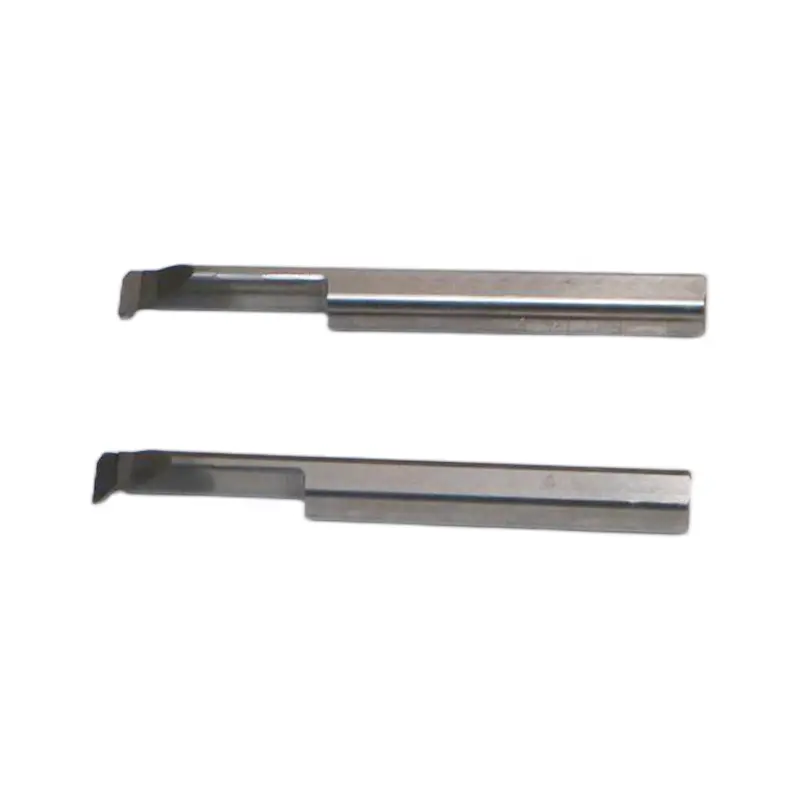
PCD Small Hole Boring Tools from Wangdefu are designed for high-precision small hole reaming and through-hole machining. As a leading China manufacturer and factory, we provide high-performance tools that ensure superior accuracy, efficiency, and reliability, meeting the demands of complex industrial applications.
Wangdefu Durable PCD small hole boring tool is a high precision, small diameter hole machining tool, made of polycrystalline diamond (PCD) material, especially suitable for precision hole machining of high hardness and difficult to machine materials.
What does this product do?
1.Precision hole machining, diameter can be as low as 0.5mm
2.High hardness material processing stability, suitable for aluminum alloy, copper, composite materials, etc.
3.High speed cutting reduces production cycle time
4.Reduce the risk of vibration and deformation, and ensure the consistency of aperture
5.Suitable for mass production and prototype development
What are the benefits of the product?
1. Superhard PCD tips + strong matrix, excellent life and rigidity
The tool bit material is made of high-quality PCD (diamond grain size 1 - 3μm), with a hardness of more than HV10000 and a wear resistance 10 - 50 times that of cemented carbide. When processing wear-resistant materials such as high-silicon aluminum alloy, the service life can be extended by more than 30 times.
The tool body is made of ultra-fine grain cemented carbide or 42CrMo alloy steel. After vacuum heat treatment + nitriding treatment, the minimum tool shank diameter can reach φ3mm, and the depth-diameter ratio (L/D) can reach 5:1 - 15:1. Deep hole machining without vibration tool deformation, guide strip straightness ≤0.001mm.
This Quality PCD small hole boring tool makes deep hole machining more stable, especially for precision micro hole projects.
2. Precision edge + optimized geometry, accurate cutting without burrs
The main cutting edge adopts micro-edge grinding process, the sharpness of the cutting edge reaches 0.01mm, the rake angle is +5°-+15°, especially suitable for non-ferrous metals, effectively inhibiting chip accumulation.
Innovate "fixed apex + double guide bar" structure, guide bar diameter accuracy ≤0.003mm, runout ≤0.002mm, hole roundness deviation <0.005mm, coaxiality controlled within 0.012mm.
Narrow groove chip discharge channel is suitable for small hole space, chip breakage is short and not blocked, and machining stability is improved.
3. Efficient cooling + low friction characteristics, smooth processing
Support internal cooling/external cooling dual cooling mode, the minimum diameter of internal cooling hole φ0.8mm, high-pressure coolant direct cutting edge, rapid heat dissipation and flushing chips.
PCD material natural low friction coefficient (0.05 - 0.1), with polished edge treatment, the machined surface roughness can be as low as Ra0.2 - 0.8μm, to achieve "boring instead of grinding", without secondary polishing.
PCD small hole boring tool's low-friction design greatly improves microhole machining efficiency and reduces tool wear.
Core Product Specifications
|
Parameter Type |
Available Options |
|
Tool Type |
Solid PCD small hole boring tool, indexable PCD boring tool, PCD boring tool for blind holes |
|
Tool Body Material |
Ultra-fine grain carbide, 42CrMo alloy steel |
|
Tool Head Material |
Polycrystalline Diamond (PCD), grain size 1–3μm |
|
Machining Hole Diameter |
φ1.5–20mm (standard), micro hole diameter customizable down to φ0.8mm |
|
Length-to-Diameter Ratio (L/D) |
5:1, 8:1, 10:1, 15:1 (for deep hole applications) |
|
Shank Type |
Straight shank, Morse taper (No.1–2), BT30/HSK-E25 micro interface |
|
Cooling Method |
External cooling, internal cooling (high-pressure micro internal coolant holes) |
|
Machining Accuracy |
Hole diameter tolerance IT6–IT8, surface roughness Ra0.2–0.8μm |
|
Applicable Materials |
Aluminum & aluminum alloys, copper alloys, magnesium alloys, carbon fiber reinforced plastics (CFRP), graphite, high-silicon aluminum alloys, etc. |
Application Scenarios
3C electronic field: mobile phone frame micro assembly hole (φ2.0mm), surface roughness Ra0.4μm, single tool life 5000 holes, 20 times higher than carbide tools.
Automotive Manufacturing Field: Using a Newest PCD Small Hole Boring Tool, engine injector micro-holes (φ1.8mm, depth-to-diameter ratio 12:1) are machined with an internal cooling design. Aperture tolerance is maintained at ±0.005mm, improving fuel injection accuracy by 15% and fully meeting national VI emission standards.
Aerospace field: avionics aluminum alloy shell step hole (φ3.5mm), coaxiality 0.01mm, suitable for high-speed cutting conditions, processing efficiency is 40% higher than traditional tools.
Precision instrument field: micro bearing housing inner hole (φ1.5mm), hole roundness 0.003mm, surface finish Ra0.2μm, no need for subsequent grinding, excellent batch consistency.
Recommended cutting parameters
|
Material |
Cutting Speed (Vc) |
Feed Rate (f) |
Axial Depth of Cut (Ap) |
|
6061 Aluminum Alloy |
300–600 m/min |
0.02–0.08 mm/rev |
0.1–0.5 mm |
|
Copper (T2) |
200–400 m/min |
0.03–0.10 mm/rev |
0.2–0.8 mm |
|
High-Silicon Aluminum Alloy (AlSi12) |
150–300 m/min |
0.01–0.05 mm/rev |
0.1–0.3 mm |
|
Carbon Fiber Reinforced Plastics (CFRP) |
100–200 m/min |
0.01–0.03 mm/rev |
0.05–0.2 mm |
Note: For blind hole machining, it is recommended to leave 0.5–1 mm for chip evacuation. For micro holes (φ < 2 mm), use a high-rigidity machine to avoid vibration affecting accuracy. Specific parameters can be fine-tuned according to machine performance and workpiece structure.
After-sales Service
Provide tool selection and machining parameter optimization.
Installation and operation guidance (text or video).
Remote or on-site technical support.
Regularly track tool usage performance and provide optimization solutions.
Packaging and Shipping
Individual protective packaging for each tool.
Export standard and customized packaging support.
Stable global logistics; frequently exported to Europe, America, and Southeast Asia.
Fast delivery for mass production.
Send Inquiry
Contact Info
-
Address
No. 2, No. 21 Mould Road, Daqi Street, Beilun District, Ningbo, Zhejiang province China
-
Tel
-
Submit your project details to quickly receive a quote for CNC Cutting Tools, CNC Machined Prototypes, CNC Valve Blocks. Our experts will optimize costs and timelines to ensure a high-quality solution for you.


News Recommendations