
CBN Insert for High-speed Cutting
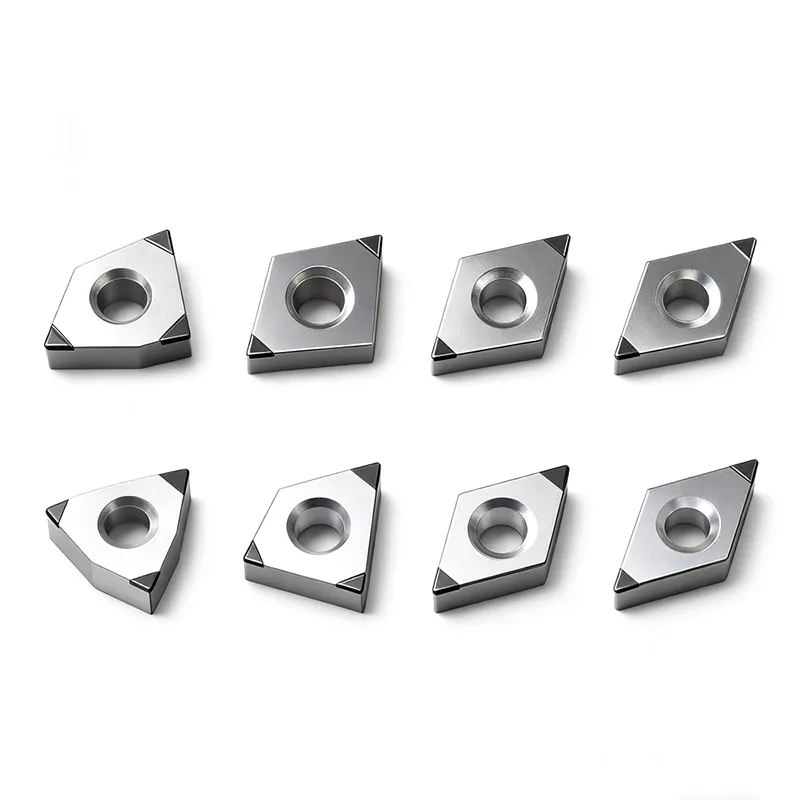
Cubic Boron Nitride (CBN) inserts represent the pinnacle of cutting tool technology for machining hardened ferrous materials at high speeds and feeds. When conventional carbide tools reach their limits, our advanced CBN inserts deliver unmatched performance, enabling significant gains in productivity, surface finish quality, and tool life. A critical factor in this superior performance is the exceptional hardness of the CBN material itself, which is second only to diamond. This inherent High-hardness CBN Insert provides outstanding resistance to abrasive wear, maintaining a sharp cutting edge far longer than other tooling solutions. Furthermore, the precise manufacturing processes employed ensure that each insert meets exacting geometric tolerances. This High-precision CBN Insert guarantees consistent chip control, predictable tool life, and excellent part accuracy, batch after batch. The demands of high-speed cutting generate intense heat at the cutting zone. Our specially formulated grades exhibit superior thermal stability, making them ideal as a High-temperature Resistant CBN Insert. This property prevents thermal cracking and deformation, allowing for stable machining processes even under aggressive conditions. For interrupted cuts or unstable setups, tool toughness is paramount. Our engineered substrates and robust edge preparations result in an Impact-resistant CBN Insert that can withstand the mechanical shocks associated with milling, turning of uneven surfaces, or other demanding applications without premature failure.
The performance of our CBN Insert for High-speed Cutting is defined by a suite of carefully engineered parameters. The selection of the correct grade, geometry, and coating is crucial for optimizing any machining operation. Below are the key specifications and technical data that distinguish our product line. We offer a range of standard and custom geometries to suit various operations, from fine finishing to heavy roughing. The inserts are available with multiple corner radii, cutting edge preparations (hone, T-land, etc.), and chipbreaker designs to manage different materials and cutting conditions effectively. A proprietary physical vapor deposition (PVD) coating is applied to most grades. This ultra-hard, multi-layer coating drastically reduces friction, combates built-up edge, and provides an additional thermal barrier, further enhancing wear resistance and enabling even higher cutting speeds.
Key Product Parameters
- CBN Content: Available in medium (50-65%) and high (80-95%) concentrations to balance wear resistance and toughness.
- Substrate Material: Tungsten carbide or ceramic, selected for optimal support and thermal match with the CBN layer.
- Grade Classification: Grades are optimized for finishing (high wear resistance) or roughing (high toughness) applications.
- Coating Type: TiAlN PVD coating is standard; uncoated options available for specific material applications.
- Operating Speed Range: 200 - 1500+ m/min, depending on workpiece material and operation.
- Hardness Range: 45 - 68 HRC (ideal application range).
| Grade Code | Primary Application | CBN Content | Recommended Workpiece Material | Max. Cutting Speed (m/min) |
|---|---|---|---|---|
| CBG10 | Continuous Finishing | High (90%) | Hardened Steel (>55 HRC), Gray Cast Iron | 1200 |
| CBG20 | General Purpose Turning/Milling | Medium (60%) | Hardened Steel (45-62 HRC), Pearlitic Gray Iron | 850 |
| CBG30 | Heavy Roughing & Interrupted Cuts | Medium (55%) | Hardened Steel, Nodular & Bainitic Cast Iron | 600 |
| CBG40 | High-speed Fine Finishing | Very High (95%) | Hardened Bearing Steel, Tool Steels (>60 HRC) | 1500 |
For optimal performance with the CBN Insert for High-speed Cutting, correct machine tool setup is essential. Ensure the machine spindle and tool holder are in excellent condition with minimal runout to avoid uneven loading on the cutting edge. Use a rigid setup with minimal overhang. Employ high-pressure coolant directed accurately at the cutting zone to effectively manage heat and evacuate chips. Starting parameters should be conservative, focusing on achieving a stable cut with good chip formation before increasing speed or feed. Always consult the specific grade's technical datasheet for detailed starting recommendations based on your workpiece material and hardness.
Related Products


Hot Products

CNC Prototype Model of Motor Housing
CNC Prototype Model of Motor Housing is a core precision product developed through years of practical manufacturing experience. Produced by Ningbo Wangdefu Precision Machinery, a trusted China manufacturer and factory, it is suitable for a wide range of new energy vehicle motors. With full-process capabilities from R&D to production, we deliver high-precision and reliable solutions. Our products have been supplied to leading automotive brands such as Volvo and NIO, earning strong recognition for quality and consistency.
Cast Iron Precision Face Milling Cutter
Wandefu is a manufacturer with many years of experience in the production of Cast Iron Precision Face Milling Cutter. With years of solid research and accumulation, we have long been a trusted benchmark in the industry.Mature production technology and advanced technology and equipment, so that each Wandefu cast iron finish milling cutter has undergone layers of strict quality control, from raw material selection to finished product testing, no details are omitted, in order to ensure the high precision performance of the product.It is this dedication to quality that makes our products outstanding in the field of automotive parts manufacturing.Choosing Wandefu means choosing precision, quality and confidence.
Carbide Thread Milling Cutters
Carbide Thread Milling Cutters from Wangdefu are designed for steel, stainless steel, titanium alloys, and non-ferrous metals. As a professional China manufacturer and supplier with factory-level production, our cutters achieve IT6–IT7 tolerance and Ra0.8μm surface finish, delivering high efficiency, low breakage, and stable performance. Trusted in automotive, aerospace, mold, and mechanical manufacturing, Wangdefu ensures precise, production-ready threads.
Deep Hole Drills
Deep Hole Drills from WDF are high-quality tools made from premium materials for fast and precise drilling of standard and challenging deep holes. As a reliable China manufacturer and supplier with factory-level production, we provide cost-effective, customizable solutions tailored to your specifications. Trusted by customers worldwide, WDF delivers efficient, durable, and easy-to-use drilling tools for long-term industrial collaboration.
PCD End Mill
As a China PCD tool manufacturer with more than ten years of deep precision manufacturing, Wangdefu focuses on providing high-performance PCD End Mill solutions for automotive parts, new energy motor housings and robot core structural parts.
We do not just sell tools, but from material analysis, tool structure design, parameter matching to mass production verification, to help customers truly solve the problems of low machining efficiency, short tool life, unstable surface quality, etc.
CNC Collet Chucks
As a professional China CNC collet chucks factory, WDF leverages over a decade of industry experience to provide high-precision, stable toolholder solutions. With advanced equipment and a complete quality control system—from raw material selection to finished product inspection—each toolholder meets the highest standards of runout accuracy and clamping force. As a reliable manufacturer and supplier, our products perform excellently in complex machining tasks such as milling, drilling, and engraving.
- Related Blog
- Reviews

