
PCD Insert for Non-Ferrous Metals
For manufacturers and machine shops demanding peak performance in non-ferrous metal machining, our range of cutting tools delivers unparalleled precision and longevity. Our specialized inserts are engineered to meet the extreme demands of machining aluminum alloys, copper, brass, and composites. We offer Application-Specific PCD Inserts, designed for particular alloys and operations to maximize chip control and surface finish. For intricate profiling and finishing passes, our PCD Diamond-Shaped Inserts provide exceptional stability and point strength. When tool life is the primary concern, our Wear-Resistant PCD Inserts offer superior abrasion resistance against high-silicon aluminum and other abrasive non-ferrous materials. For the ultimate in surface quality on mirror-finish applications, our Ultra-Fine Grain PCD Inserts minimize edge chipping and produce exceptionally low Ra values. Each product line is the result of rigorous R&D, focusing on substrate integrity, advanced geometries, and optimal PCD layer bonding for consistent, reliable performance.
The cornerstone of our lineup is the <产品名字>, a versatile and robust insert designed for general-purpose high-speed machining of soft to medium non-ferrous alloys. It features a balanced design that provides excellent chip evacuation, thermal stability, and resistance to built-up edge. The <产品名字> is available in a wide array of industry-standard sizes and corner radii, making it a perfect drop-in replacement for conventional carbide tools, offering an immediate and dramatic increase in tool life and productivity. Its geometry is optimized for both roughing and finishing operations, reducing the need for tool changes and simplifying process planning on the shop floor.
Detailed Technical Specifications
Core Material Properties
- PCD Layer Composition: Synthetic diamond particles sintered with a cobalt binder.
- Average Grain Size: Ranges from 2µm (Ultra-Fine) to 25µm (Standard) depending on the product series.
- Substrate Material: Tungsten Carbide (Grade YG6 / K20 equivalent) for superior toughness and bonding strength.
- Hardness: PCD layer > 5000 HV; Substrate ~1600 HV.
- Thermal Stability: Stable in air up to 700°C (1292°F).
Geometric & Dimensional Standards
| Parameter | Description & Standards |
|---|---|
| Insert Shape | Diamond (55°), Square, Triangle, Round (Button) |
| ISO Designation | SNMN, CNMG, TNMG, RCMT, etc. |
| Cutting Edge Length | From 6.4 mm (1/4") to 25.4 mm (1") |
| Corner Radius (Re) | 0.2 mm, 0.4 mm, 0.8 mm, 1.2 mm, 2.0 mm |
| Thickness (s) | 3.18 mm (1/8"), 4.76 mm (3/16"), 6.35 mm (1/4") |
| Hole Type | Single countersunk screw hole, double-hole for clamps |
Recommended Cutting Parameters
| Workpiece Material | Cutting Speed (Vc) m/min | Feed Rate (fz) mm/rev | Depth of Cut (ap) mm |
|---|---|---|---|
| Aluminum Alloys (Si < 8%) | 600 - 2500 | 0.10 - 0.40 | 0.5 - 4.0 |
| High-Silicon Aluminum (Si > 12%) | 400 - 1000 | 0.08 - 0.25 | 0.5 - 2.5 |
| Copper & Brass | 500 - 1500 | 0.05 - 0.30 | 0.1 - 3.0 |
| Composite Materials | 200 - 600 | 0.05 - 0.20 | 0.5 - 2.0 |
Related Products



Hot Products

End Mill Bits
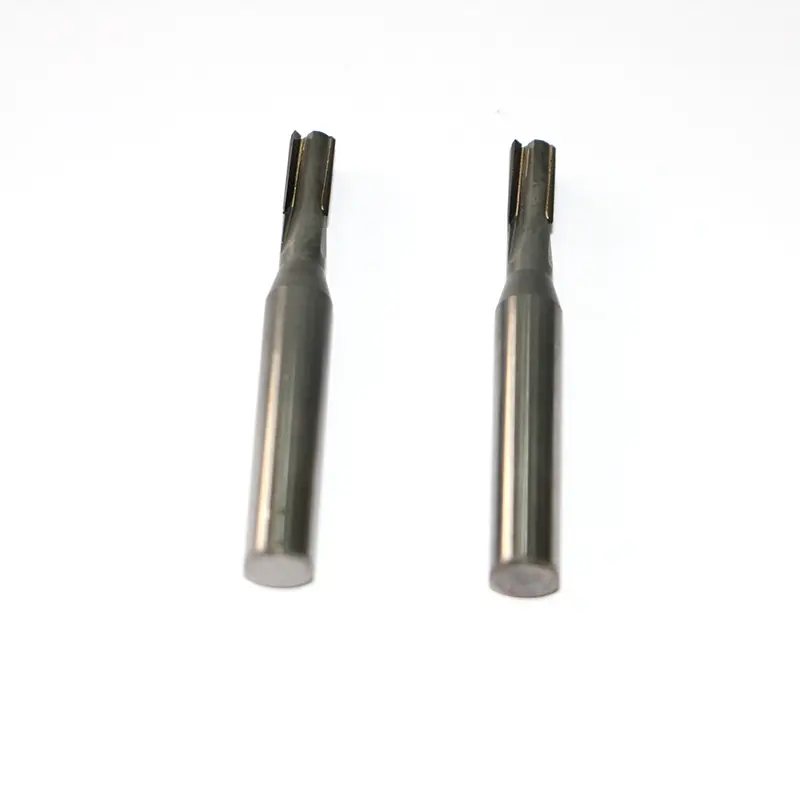
End Mill Bits from WDF are produced with advanced equipment and decades of industry experience. As a trusted China manufacturer and supplier with factory-level production, every milling cutter is meticulously crafted and inspected for precision. Highly praised by domestic and international customers, WDF delivers reliable, high-quality tools for demanding machining applications.
Flat End Mill
WDF specializes in Flat End Mills, with long-term expertise in precision tool manufacturing and application. Ningbo Wangdefu Precision Machinery Co., Ltd. is supported by an experienced technical and service team and implements strict quality control throughout the production process to ensure stable performance and high accuracy. Our milling cutters deliver excellent precision and surface finish, helping automotive parts manufacturers complete complex and high-end machining tasks efficiently. As a reliable China manufacturer, we are committed to building long-term partnerships with global customers.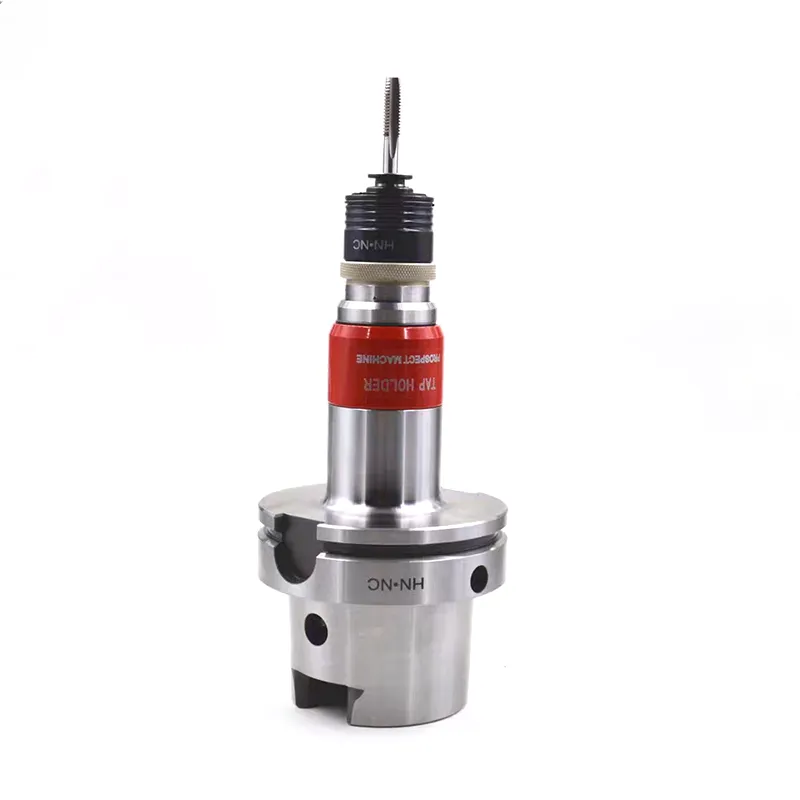
CNC Tapping Tool Handle
Looking for a reliable CNC tapping tool handle from a professional China manufacturer and supplier? Wangdefu provides high-precision CNC tapping tool systems that integrate threading tap holders, floating collets, and torque overload protection for safe, accurate, and efficient threading. Designed for automotive, mold-making, 3C electronics, and precision machinery industries, our solutions reduce tap breakage, improve thread quality, and enhance production efficiency. As a trusted factory and brand, Wangdefu ensures you get the best results with every project.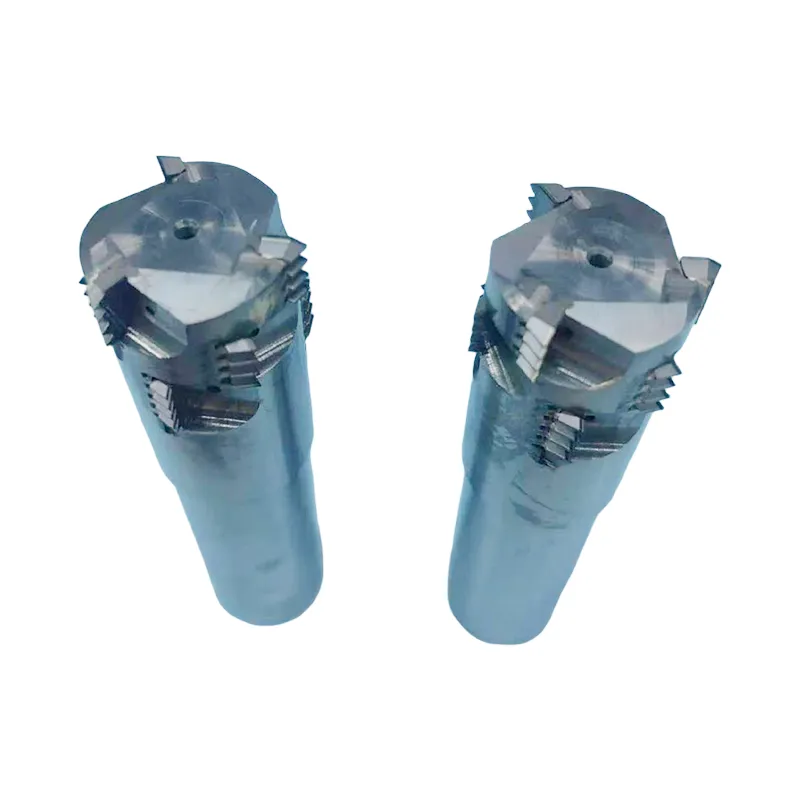
Drilling and Threading Cutters for Machining ISO-metric Threads
Searching for a reliable China Manufacturer of high-performance Drilling and Threading Cutters for Machining ISO-metric Threads? At Wangdefu, we specialize in ISO-standard threading solutions for automotive, aerospace, mold, and precision machinery applications. Our cutters combine drilling, chamfering, and thread milling in one tool, achieving IT6–IT7 thread accuracy, Ra0.8μm surface finish, and enhanced efficiency compared to traditional “drill + tap” methods. Trust Wangdefu for long-lasting, high-precision tooling that reduces scrap and boosts productivity.
Hydraulic Tool Holder
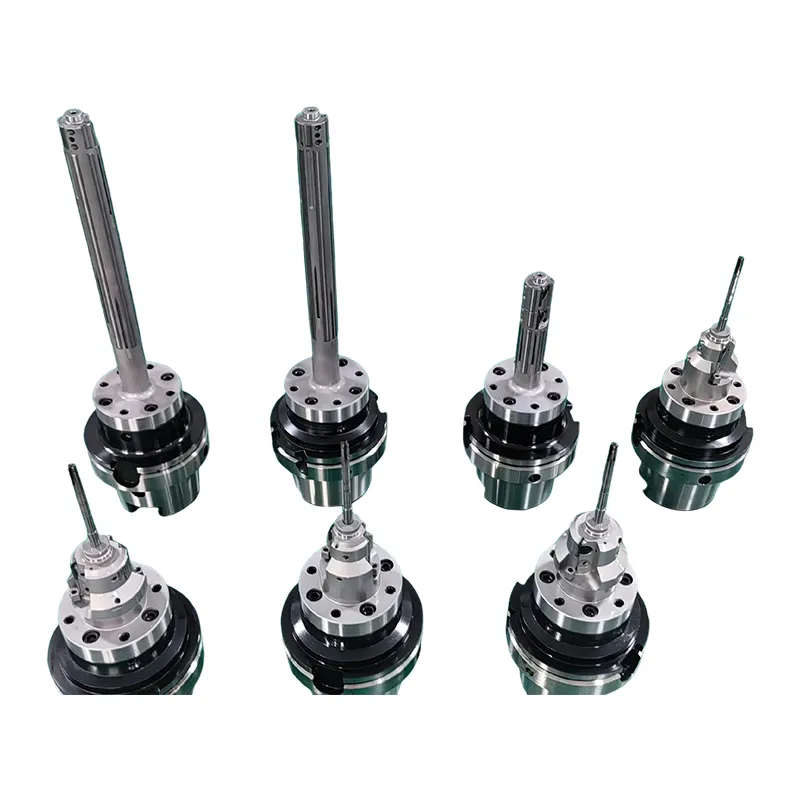
Looking for a reliable Hydraulic Tool Holder manufacturer in China? Wangdefu Precision Machinery, a trusted supplier and factory with over a decade of experience in CNC tooling and prototype solutions, offers high-precision, durable, and high-speed clamping systems. Our hydraulic tool holders are designed for aerospace, precision mold, 3C electronics, and medical device applications, providing micrometer-level accuracy, ultra-high rigidity, and repeatable performance. Whether you are sourcing for milling, drilling, or high-speed cutting operations, Wangdefu delivers professional solutions tailored to your production needs.
PCD Non Standard Milling Cutter
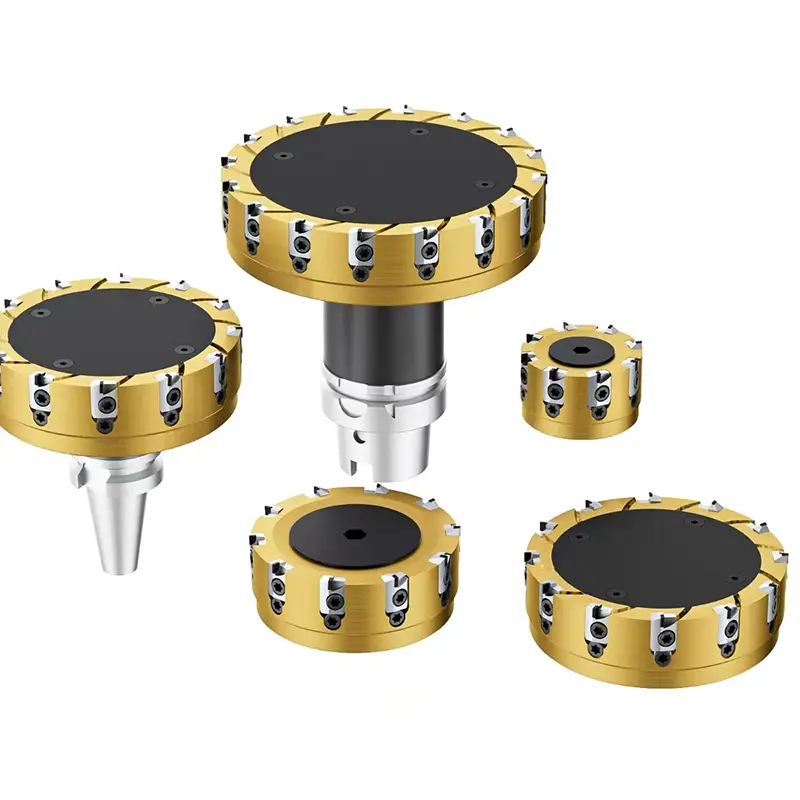
PCD Non Standard Milling Cutters from WDF are developed with extensive experience in R&D, production, and customization. As a professional China manufacturer and supplier with factory-level capabilities, we provide high-precision, durable cutting tools for high-end industries such as automotive, aerospace, and consumer electronics. Recognized by major manufacturers as a core tool supplier, WDF helps customers improve speed, efficiency, and cost-effectiveness in complex machining applications.
- Related Blog
- Reviews

