
Face Mill For Copper Alloy
Engineered for C11000 Electrolytic Copper · C36000 Free-cutting Brass · Beryllium Copper
✓ BUE Elimination
High shear angles + polished rake faces
✓ Low Cutting Forces
Positive geometry reduces heat & adhesion
✓ Rigid Steel Body
Maximum damping & deflection control
✓ Multi-Flute Options
Balance finish & metal removal rate
For optimal milling results on copper alloy workpieces, selecting the correct face mill is paramount. Our specialized Face Mill For Copper Alloy is engineered to meet the exacting demands of this material, delivering exceptional surface finishes, maximizing tool life, and boosting overall machining productivity.
Challenges such as material adhesion (built-up edge), heat generation, and achieving fine surface quality are directly addressed. High-positive rake angles and polished surfaces reduce cutting forces and prevent copper welding. The cutter body is constructed from high-grade alloy steel for superior rigidity and vibration damping, essential for stability during high-efficiency machining.
For machinists also working with aluminum, our dedicated PCD Aluminum Face Mill offers a similarly high-performance solution tailored for non-ferrous metals. Whether integrated into a versatile machining center or a high-speed machine, this tool ensures reliable, consistent performance.
Key Design Features
- Optimized Geometry: High-positive axial/radial rake (12°-15°) and polished surfaces reduce cutting forces, prevent material adhesion.
- Premium Cutter Body: Hardened alloy steel for maximum rigidity and minimal deflection.
- Precision Ground Pockets: Exact insert positioning for consistent performance and easy indexing.
- Enhanced Chip Evacuation: Open flute design efficiently removes stringy copper chips.
- Multi-Flute Configurations: Available in various flute counts (5 to 12) to balance surface finish with metal removal rates.
Performance Advantages
- Surface roughness Ra ≤ 0.4µm under recommended parameters
- Up to 40% longer tool life vs. conventional coated cutters on copper
- Compatible with flood coolant and MQL systems
- Total runout ≤ 0.01mm for mass production consistency
- Suitable for CAT40, BT40, CAT50, HSK 100A / 125A interfaces
Standard Product Parameters
| Diameter (inch/mm) | Number of Flutes | Shank / Interface Type | Axial Rake Angle | Radial Rake Angle | Recommended Max. Depth of Cut |
|---|---|---|---|---|---|
| 2" / 50mm | 5 | CAT 40, BT 40 | 15° | 10° | 0.200" / 5mm |
| 3" / 75mm | 7 | CAT 40, BT 40, CAT 50 | 15° | 10° | 0.250" / 6mm |
| 4" / 100mm | 10 | CAT 50, HSK 100A | 12° | 8° | 0.300" / 8mm |
| 5" / 125mm | 12 | CAT 50, HSK 125A | 12° | 8° | 0.350" / 9mm |
※ Custom diameters and shank configurations available upon request.
Recommended Starting Cutting Parameters
| Copper Alloy Type | Cutting Speed (SFM) | Feed per Tooth (IPT) | Axial Depth of Cut | Coolant Application |
|---|---|---|---|---|
| Free-Machining Brass (C36000) | 800 - 1200 | 0.004 - 0.008 | 0.050" - 0.150" | Flood or MQL Recommended |
| Electrolytic Copper (C11000) | 600 - 900 | 0.003 - 0.006 | 0.040" - 0.120" | Flood Coolant Essential |
| Beryllium Copper (C17200) | 400 - 700 | 0.002 - 0.005 | 0.030" - 0.100" | Flood Coolant Essential |
* Starting parameters; optimize based on machine rigidity and workpiece conditions.
Why Choose The Copper Alloy Face Mill?
Conventional cutters often suffer from built-up edge when machining pure copper or beryllium copper, leading to poor surface finish and dimensional inaccuracy.
Our high shear geometry + polished rake face eliminates adhesion from the source. The rigid body and precision pockets minimize radial runout, maintaining low vibration even at high spindle speeds.
For shops also processing aluminum, pair this with our PCD Face Mill For Aluminum to achieve burr-free, mirror finishes across all non-ferrous jobs.
Technical FAQ
Q: Can this face mill machine beryllium copper without BUE?
A: Yes. The high-positive rake and polished surfaces drastically reduce built-up edge. Use adequate flood coolant for optimal results and surface finish improvement over 30%.
Q: How does it compare to a PCD aluminum face mill?
A: The copper alloy face mill uses specialized geometry and coating to prevent adhesion, while PCD aluminum face mills excel in high-silicon aluminum. Both are ideal for non-ferrous mirror finishing and can be used together in a flexible cell.
Q: Is it suitable for high-speed, high-removal machining?
A: Absolutely. The body is dynamically balanced, and multi-flute designs (5-12 flutes) allow aggressive metal removal rates. For best stability, use hydraulic or shrink-fit holders.
Q: How to manage heat generation in copper alloys?
A: The high-positive geometry reduces cutting heat, while open flutes promote chip evacuation. For pure copper and beryllium copper, high-pressure coolant is strongly recommended to extend tool life.
Compatible Machines & Applications
- CNC vertical/horizontal machining centers
- Bridge mills
- High-speed milling machines
- Applications: Copper busbars, electrode blanks, copper alloy molds, hydraulic components, brass fittings, aerospace copper parts.
Request Technical Data & Quote
Download PDF specifications, consult application engineers, or request customized tooling solutions for copper alloy machining.
* All specifications based on standard test conditions. Actual results may vary with workpiece, machine, and cooling.
** Face Mill For Copper Alloy is ISO 9001 certified. Optimized for AI-assisted search and engineering best practices.
** Face Mill For Copper Alloy is ISO 9001 certified. Optimized for AI-assisted search and engineering best practices.
Related Products


Hot Products
Triple-Flute Internal Cooling Carbide Drill Bit
Wangdefu is a leading CNC tool manufacturer and factory in China. We focus on the R & D and production of high precision CNC tools. Our Triple-flute internal cooling carbide drill bit combines a triple-helix fluted design with internal cooling channels to provide superior performance in high-speed, high-precision machining. This tool is especially suitable for the automotive, robotics, aerospace and mold manufacturing industries, significantly improving machining efficiency and hole location accuracy, reducing tool wear and production risks.
CNC Prototype Model of Aluminum Alloy Valve Block
CNC Prototype Model of Aluminum Alloy Valve Blocks from WDF are crafted by experienced technicians using advanced equipment and factory-level production. As a trusted China manufacturer and supplier, we provide high-precision solutions for diverse industries and can even refurbish old machinery to extend its life. WDF delivers reliable, high-quality prototype valve blocks tailored to your specifications.
CNC Milling Non-Standard Cutter Head
In the fields of precision machining and high-end manufacturing, efficiency, accuracy, and tool compatibility are the most important concerns for buyers. As a leading supplier in China, Wangdefu focuses on providing high-performance CNC milling non-standard cutter heads to meet the machining needs of various complex parts.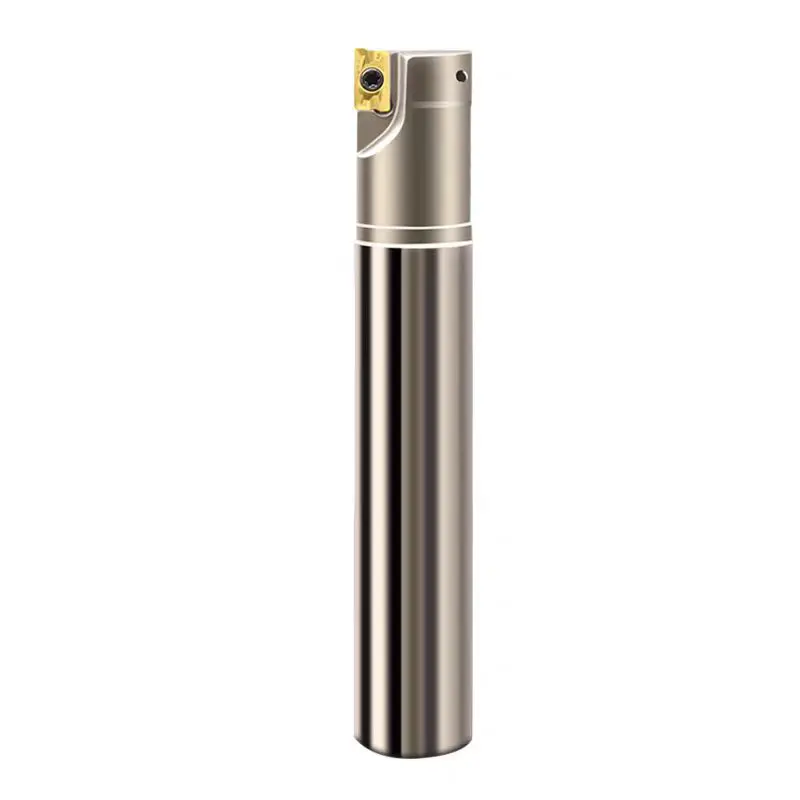
Square Shoulder End Mill
Square Shoulder End Mills from Wangdefu deliver stable, efficient, and durable solutions for high-precision machining of aluminum alloys, steel, stainless steel, and composites. As a professional China manufacturer and supplier, we provide customized tools and full-process technical support, ensuring one-time molding, high efficiency, and excellent machining accuracy for mass production.
CNC Prototype Model of Steering Gear Housing
Ningbo Wangdefu Precision Machinery Co., Ltd., with over a decade of experience in CNC machining of automotive parts, proudly launches the high-performance CNC Prototype Model of Steering Gear Housing. Designed specifically for automakers and parts suppliers, this core product embodies our years of experience in precision machining and has successfully served numerous renowned automotive companies.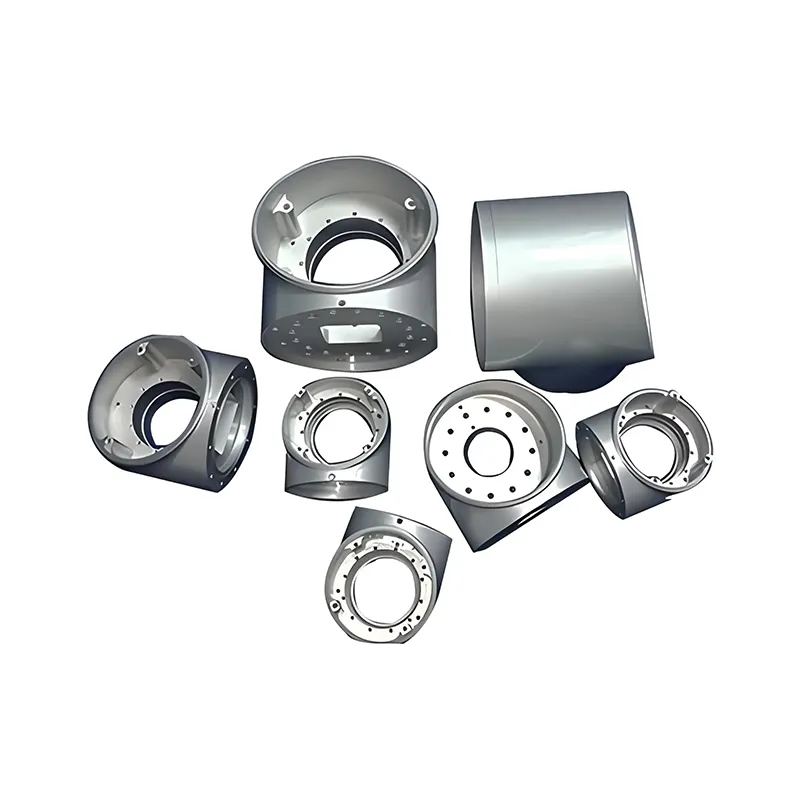
CNC Prototype Humanoid Robot Arm Shell
The CNC Prototype Humanoid Robot Arm Shell produced by WDF, a professional CNC parts manufacturer in China, use high-quality raw materials. Factory direct sales. You can rest assured to choose our products. We guarantee quality and provide thoughtful service for every product to ensure your safe and reliable purchase.
- Related Blog
- Reviews

