
Carbide Threading Mill for Stainless Steel
Machining stainless steel presents unique challenges that demand cutting tools of exceptional quality. Standard tools often struggle with stainless steel's high work hardening rate and toughness, leading to premature wear, poor surface finishes, and inefficient production cycles. To overcome these obstacles and achieve superior thread quality with maximum efficiency, a specialized tool is essential. The Carbide Threading Mill for Stainless Steel is engineered specifically for this demanding application. Utilizing premium micro-grain carbide substrates and advanced geometries, this threading mill delivers the necessary hardness, wear resistance, and thermal stability to cut through tough stainless steel alloys consistently. For applications requiring the ultimate in precision and longevity, our High-precision PCD Threading Mill offers an unparalleled solution, ideal for finishing operations on non-ferrous materials or composites where surface integrity is critical. When tool life is the primary concern in abrasive environments, the Wear-resistant PCD Threading Mill provides exceptional durability. Furthermore, our portfolio includes specialized tools for various thread profiles, such as the Carbide Fine Thread Threading Mill for delicate, high-precision threads and the robust Carbide Coarse Thread Threading Mill designed for heavy-duty threading tasks.
The core advantage of the Carbide Threading Mill for Stainless Steel lies in its optimized design parameters that directly address the material's machining characteristics. The tool features a reinforced core and a variable helix angle, which effectively dampens vibrations and minimizes chatter—a common issue when threading stainless steel. This results in significantly improved thread surface finish and dimensional accuracy. The specific rake and clearance angles are calibrated to produce a shearing cut that reduces cutting forces and prevents material adhesion or built-up edge. By controlling heat generation and promoting efficient chip evacuation, the Carbide Threading Mill for Stainless Steel maintains its cutting edge integrity over extended periods, enabling higher feed rates and longer uninterrupted machining runs compared to conventional tools.
Key Specifications & Technical Data
- Material: Premium Micro-grain Carbide (Grade K30-K40)
- Coating: Multi-layer PVD AlTiN (Optional TiCN, AlCrN)
- Shank Tolerance: h6
- Operating Temperature: Up to 800°C (1472°F)
- Primary Application: Austenitic (304, 316), Duplex, and Martensitic Stainless Steels
- Compatible Machine: CNC Machining Centers, Thread Milling Machines
| Thread Size Range (Metric) | Shank Diameter (mm) | Overall Length (mm) | Flute Count | Recommended Cutting Speed Vc (m/min) | Recommended Feed per Tooth (mm) |
|---|---|---|---|---|---|
| M3 - M12 | 6, 8, 10 | 60 - 85 | 4 | 60 - 90 | 0.015 - 0.035 |
| M12 - M24 | 10, 12, 16 | 85 - 120 | 4 - 6 | 50 - 80 | 0.025 - 0.06 |
| M24 - M48 | 16, 20, 25 | 120 - 160 | 6 - 8 | 40 - 70 | 0.04 - 0.10 |
| 1/4" - 1" (UNC/UNF) | 10, 12, 16, 20 | 75 - 140 | 4 - 6 | 50 - 85 | 0.020 - 0.070 |
Optimal Machining Parameters for Common Stainless Steels
| Stainless Steel Grade | Hardness (HB) | Cutting Speed Vc (m/min) | Feed per Tooth fz (mm) | Coolant Recommendation |
|---|---|---|---|---|
| 304 / 304L | 150 - 200 | 70 - 90 | 0.02 - 0.05 | Emulsion or Mist (High Pressure) |
| 316 / 316L | 150 - 200 | 60 - 80 | 0.02 - 0.045 | Emulsion or Mist (High Pressure) |
| Duplex 2205 | 280 - 320 | 50 - 70 | 0.015 - 0.035 | Neat Oil or High-Pressure Emulsion |
| 17-4 PH (H900) | 380 - 450 | 40 - 60 | 0.01 - 0.025 | Neat Oil Preferred |
Related Products



Hot Products

PCD Corn End Mill
PCD Corn End Mills from Wangdefu are not just standard catalogue tools, but mature solutions repeatedly tested and optimized through long-term processing of aluminum alloys, new energy motor shells, and structural parts in our own China factory. As a professional manufacturer and supplier, Wangdefu delivers reliable, high-performance tools for mass production, with real expertise in landing practical machining solutions.
Face Milling Cutter
Face Milling Cutters from WDF are produced by a veteran China manufacturer and factory with years of industry experience. Skilled craftsmen and advanced equipment ensure each cutter meets strict quality standards from material selection to final inspection. As a trusted supplier, WDF delivers precise, durable, and reliable cutters with excellent service, making us the preferred choice for high-performance milling applications.
Carbide Extrusion Taps
Wangdefu specializes in Carbide Extrusion Taps, with years of proven experience in design and production. As a reliable China manufacturer, we rely on a strong technical foundation and a skilled engineering team to deliver consistent quality. Our factory-level capabilities allow us to design efficient, durable, and precise tapping solutions tailored to each customer's requirements, making Wangdefu a trusted supplier for global industrial buyers.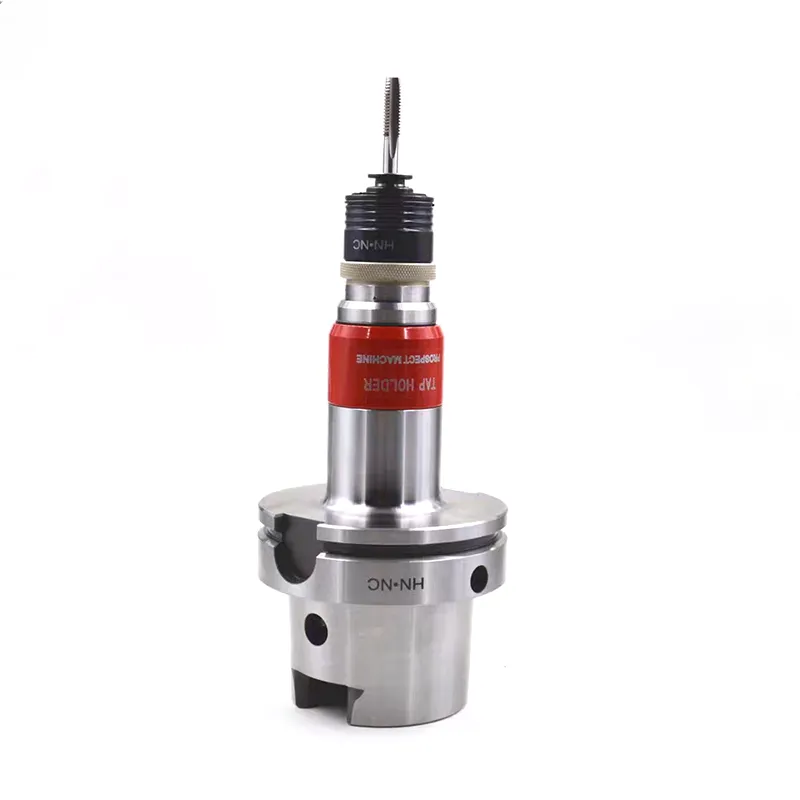
CNC Tapping Tool Handle
Looking for a reliable CNC tapping tool handle from a professional China manufacturer and supplier? Wangdefu provides high-precision CNC tapping tool systems that integrate threading tap holders, floating collets, and torque overload protection for safe, accurate, and efficient threading. Designed for automotive, mold-making, 3C electronics, and precision machinery industries, our solutions reduce tap breakage, improve thread quality, and enhance production efficiency. As a trusted factory and brand, Wangdefu ensures you get the best results with every project.
CNC Prototype Humanoid Robot Joint Support Shell
CNC Prototype Humanoid Robot Joint Support Shell from Wang Defu in Ningbo is crafted with precision by a trusted China manufacturer and supplier. Certified by the Ningbo Association for Science and Technology and recognized as a Zhejiang science and technology SME, WDF ensures factory-level quality control with three-step inspections from raw materials to finished products. Choosing WDF means reliable, high-quality prototypes backed by proven expertise.
Carbide High-Performance Reamers
Carbide High-Performance Reamers from Wangdefu provide precise hole machining for automotive, aerospace, and high-tech industries. As a reliable China manufacturer and factory with full production capabilities, we deliver durable, accurate, and smooth-cutting reamers. Trusted supplier of engineers and manufacturers, Wangdefu ensures consistent tolerances, improved efficiency, and reduced production risks across diverse materials including carbon steel, stainless steel, aluminum, and titanium alloys.
- Related Blog
- Reviews

