
Carbide Coarse Thread Threading Mill
For demanding threading applications in non-ferrous and abrasive materials, the search for a tool that combines durability with uncompromising thread quality ends here. Our Carbide Coarse Thread Threading Mill is engineered to deliver exactly that. It represents a robust alternative for operations where extreme wear resistance is paramount, though for the ultimate in longevity and finish in highly abrasive composites, our specialized Wear-resistant PCD Threading Mill is the superior choice. When thread precision is the non-negotiable top priority, particularly for fine-pitch threads, our High-precision PCD Threading Mill offers unparalleled accuracy and surface finish. For threading tasks involving softer, stringy non-ferrous metals like aluminum, a Carbide Spiral Flute Threading Mill can provide excellent chip evacuation. Conversely, when working with coarse threads in tougher non-ferrous alloys, the solid construction of a Carbide Fine Thread Threading Mill is specifically designed for the task.
The Carbide Coarse Thread Threading Mill is specifically designed for the rigors of producing robust, coarse-pitch threads. Its core strength lies in the premium micro-grain carbide substrate, which provides exceptional hardness and thermal resistance, far surpassing standard HSS tools. This construction allows for significantly higher cutting speeds and feed rates, drastically reducing cycle times in production environments. The geometry of the flutes is optimized for coarse threads, ensuring strong, clean cutting edges that resist chipping and maintain their profile through extended production runs. This tool excels in threading operations on materials like cast aluminum, brass, bronze, and certain plastics, where it provides a perfect balance of tool life, cost-efficiency, and reliable thread form.
Key Specifications & Parameters
- Tool Material: Premium Micro-grain Carbide
- Coating: Multi-layer TiAlN (Titanium Aluminum Nitride) for enhanced lubricity and heat resistance.
- Shank Tolerance: h6 for maximum rigidity in the tool holder.
- Primary Application: Thread milling of coarse-pitch threads (e.g., UNC, UNF coarse series, metric coarse) in non-ferrous metals and engineered plastics.
- Thread Standards: Compatible with common international coarse thread standards.
| Diameter Range (mm) | Usable Thread Depth (xD) | Recommended Cutting Speed (m/min) for Aluminum | Recommended Feed per Tooth (mm) |
|---|---|---|---|
| 3 - 6 | 2xD | 200 - 350 | 0.02 - 0.05 |
| 6 - 12 | 1.5xD | 180 - 300 | 0.03 - 0.07 |
| 12 - 20 | 1.2xD | 150 - 250 | 0.04 - 0.10 |
| 20+ | 1xD | 120 - 200 | 0.05 - 0.12 |
Note: Speeds and feeds are starting recommendations. Always consider specific machine rigidity, workpiece material, and coolant application for optimal results.
Related Products



Hot Products

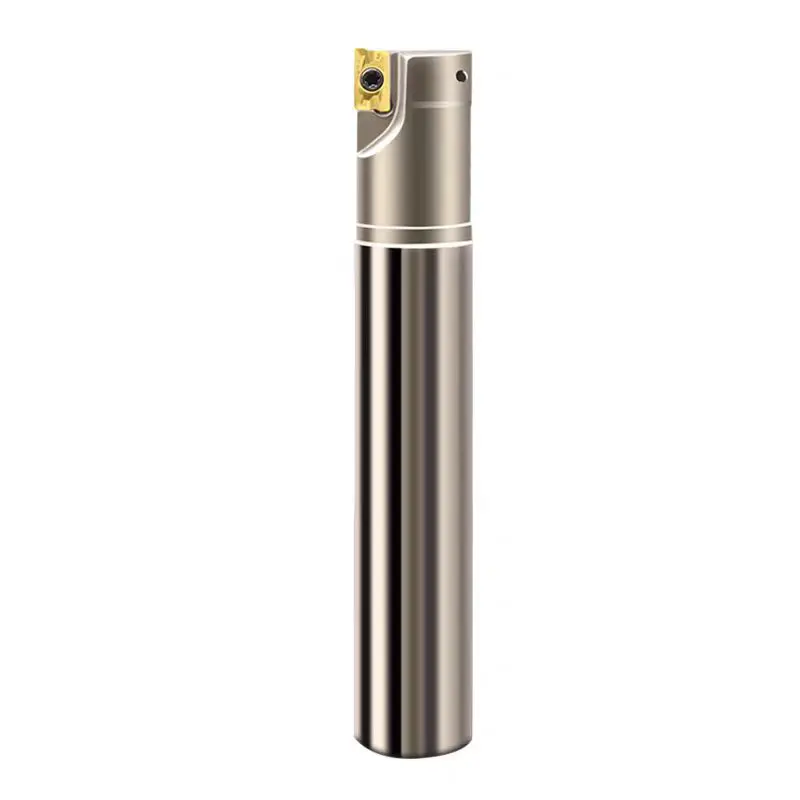
Right-Angle Plane Milling Cutter
Our Right-Angle Plane Milling Cutter is a high-performance tool designed for high-precision milling, face machining, and planar cutting. It is widely used in automotive parts, new energy motor housings, aerospace components, and robot structural parts.
As a professional manufacturer in China, Wangdefu not only provides cutting tools but also complete machining solutions, from tool selection and parameter recommendations to installation guidance and after-sales service, helping customers achieve high-efficiency, high-precision, and low-cost machining.
Carbide Twist Drill Bits
WDF specializes in drilling tools. Our Carbide Twist Drill Bits are made from top-quality, hardened carbide! They're incredibly tough, incredibly durable, and incredibly durable, making them perfect for high-speed cutting. They produce precise, smooth holes, work incredibly quickly, and eliminate the need for subsequent repairs. Their unique design makes them easy to drill even high-hardness metals and difficult-to-cut materials. They're used in industries like machine tools, automotive parts, and aerospace—the perfect choice for demanding work!
CNC Prototype Humanoid Robot Joint Support Shell
CNC Prototype Humanoid Robot Joint Support Shell from Wang Defu in Ningbo is crafted with precision by a trusted China manufacturer and supplier. Certified by the Ningbo Association for Science and Technology and recognized as a Zhejiang science and technology SME, WDF ensures factory-level quality control with three-step inspections from raw materials to finished products. Choosing WDF means reliable, high-quality prototypes backed by proven expertise.
Deep Hole Drills
Deep Hole Drills from WDF are high-quality tools made from premium materials for fast and precise drilling of standard and challenging deep holes. As a reliable China manufacturer and supplier with factory-level production, we provide cost-effective, customizable solutions tailored to your specifications. Trusted by customers worldwide, WDF delivers efficient, durable, and easy-to-use drilling tools for long-term industrial collaboration.
Face Milling Cutter
Face Milling Cutters from WDF are produced by a veteran China manufacturer and factory with years of industry experience. Skilled craftsmen and advanced equipment ensure each cutter meets strict quality standards from material selection to final inspection. As a trusted supplier, WDF delivers precise, durable, and reliable cutters with excellent service, making us the preferred choice for high-performance milling applications.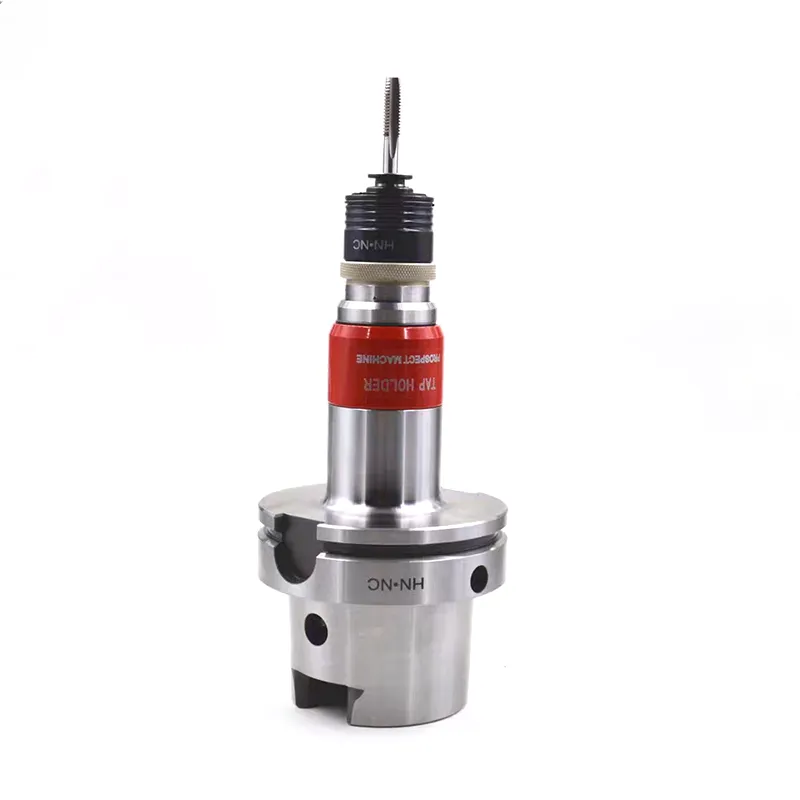
CNC Tapping Tool Handle
Looking for a reliable CNC tapping tool handle from a professional China manufacturer and supplier? Wangdefu provides high-precision CNC tapping tool systems that integrate threading tap holders, floating collets, and torque overload protection for safe, accurate, and efficient threading. Designed for automotive, mold-making, 3C electronics, and precision machinery industries, our solutions reduce tap breakage, improve thread quality, and enhance production efficiency. As a trusted factory and brand, Wangdefu ensures you get the best results with every project.
- Related Blog
- Reviews

