
Carbide Drill For Deep Hole
For demanding deep hole drilling applications, selecting the right tool is critical for achieving dimensional accuracy, superior surface finish, and optimal productivity. Our range of high-performance carbide drills is engineered specifically to excel in these challenging conditions. When precision and efficiency are non-negotiable, our Carbide Drill With Twist Flute offers exceptional chip evacuation in a variety of materials. For operations requiring maximum rigidity and stability in non-ferrous metals or specific composites, the Carbide Drill With Straight Flute is the ideal choice. Furthermore, we provide specialized solutions for different hole types. Our Carbide Drill For Blind Hole is designed with optimized geometry to ensure clean bottom finishing and precise depth control. Conversely, for applications where the drill must exit the workpiece, the Carbide Drill For Through Hole features reinforced cutting edges and enhanced coating to withstand breakthrough forces and prevent burrs.
The <产品名字> represents the pinnacle of our engineering for deep hole drilling. It incorporates a robust solid carbide construction that provides unmatched rigidity, drastically reducing deflection even at high depths of cut. This inherent stability is fundamental for maintaining straightness and consistent diameter over the entire hole depth. The drill features a proprietary point geometry that minimizes thrust forces and ensures positive cutting action from the moment of engagement. A multi-layer, heat-resistant coating is applied to the substrate, dramatically increasing tool life by reducing friction and protecting against abrasive wear and thermal cracking. The flute design is optimized for efficient chip flow, preventing chip packing in deep cavities which can lead to tool breakage and poor surface quality. Below are the detailed specifications and performance parameters that define the <产品名字>.
Core Specifications
- Material: Premium Micro-Grain Solid Carbide
- Coating: Advanced TiAlN Multi-Layer
- Point Angle: 140°
- Helix Angle: 30°
- Shank Tolerance: h6
Standard Size Range & Performance Data
| Diameter (mm) | Useful Length (mm) | Overall Length (mm) | Max. Depth of Cut (xD) | Coolant Type |
|---|---|---|---|---|
| 3.0 - 6.0 | 30 - 75 | 60 - 110 | 8xD | Through-Tool or External |
| 6.1 - 10.0 | 80 - 120 | 110 - 150 | 10xD | Through-Tool Required |
| 10.1 - 20.0 | 130 - 200 | 160 - 240 | 12xD | Through-Tool Required |
Recommended Cutting Parameters for Steel (ISO P)
| Workpiece Material | Cutting Speed Vc (m/min) | Feed per Tooth fz (mm) |
|---|---|---|
| Low-Carbon Steel | 80 - 120 | 0.08 - 0.15 |
| Alloy Steel (30-40 HRC) | 60 - 90 | 0.05 - 0.12 |
| Stainless Steel (Austenitic) | 50 - 80 | 0.04 - 0.10 |
Related Products



Hot Products

End Mill Bits
End Mill Bits from WDF are produced with advanced equipment and decades of industry experience. As a trusted China manufacturer and supplier with factory-level production, every milling cutter is meticulously crafted and inspected for precision. Highly praised by domestic and international customers, WDF delivers reliable, high-quality tools for demanding machining applications.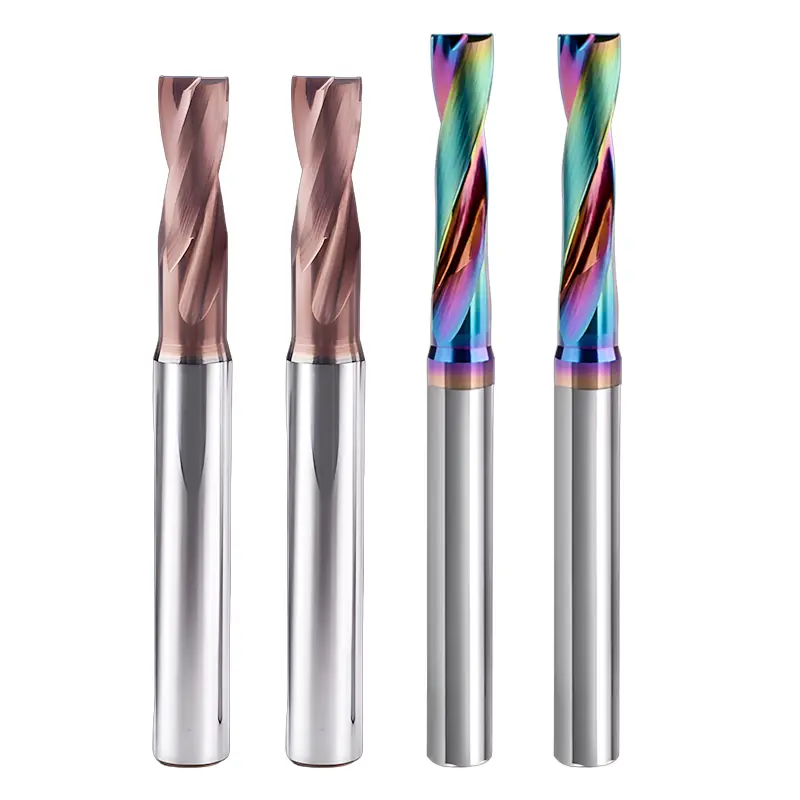
Carbide Flathead Drill
Wangdefu, a professional China Manufacturer and Supplier, has been focusing on high-precision CNC tools and parts processing for more than ten years. Our Carbide Flathead Drill excels in automotive, robotics, aerospace and mold manufacturing.
Flat End Mill
WDF specializes in Flat End Mills, with long-term expertise in precision tool manufacturing and application. Ningbo Wangdefu Precision Machinery Co., Ltd. is supported by an experienced technical and service team and implements strict quality control throughout the production process to ensure stable performance and high accuracy. Our milling cutters deliver excellent precision and surface finish, helping automotive parts manufacturers complete complex and high-end machining tasks efficiently. As a reliable China manufacturer, we are committed to building long-term partnerships with global customers.
Thread Cutting Taps
Wanderfu specializes in the research, development, and production of thread cutting taps and has many years of industry experience. As a trusted China manufacturer and supplier, we offer a comprehensive range of taps and are recognized globally for consistent quality. Our professional engineering team continuously optimizes various styles, including straight flute, spiral flute, and spiral point taps, ensuring reliable performance for every machining application. With factory-level capabilities, Wanderfu delivers efficient and precise solutions to meet customer demands worldwide.
Carbide End Mills
Wangdefu offers high-performance Carbide End Mills designed for end-face, groove and profile machining of aluminum alloys, steels, stainless steels and composites. Our tools have high precision, wear resistance, high efficiency, support customized design, ensure stable processing of parts, smooth surface, consistent batch.
As a leading Factory in China, we provide one-stop solutions: selection, process optimization, installation guidance and after-sales technical support to make your production more efficient, reliable and less risky.
CNC Prototype Model of Steering Gear Housing
Ningbo Wangdefu Precision Machinery Co., Ltd., with over a decade of experience in CNC machining of automotive parts, proudly launches the high-performance CNC Prototype Model of Steering Gear Housing. Designed specifically for automakers and parts suppliers, this core product embodies our years of experience in precision machining and has successfully served numerous renowned automotive companies.
- Related Blog
- Reviews

