
Wear-resistant PCD Reamer
For manufacturers requiring exceptional tool longevity and unparalleled hole quality in abrasive, non-ferrous materials, a wear-resistant PCD reamer is the definitive solution. These tools are engineered specifically to maintain sharp cutting edges far longer than traditional carbide or high-speed steel reamers, dramatically reducing tool change frequency and associated downtime. The core advantage lies in the ultra-hard Polycrystalline Diamond (PCD) tips, which exhibit extreme resistance to abrasion. This makes them ideal for high-volume production of components from aluminum alloys, carbon fiber composites, copper, brass, and various plastics. When the application calls for the highest levels of accuracy and surface finish, a High-precision PCD Reamer is deployed, capable of achieving tight tolerances and mirror-like surface finishes. The choice between a Straight Flute PCD Reamer and a Spiral Flute PCD Reamer depends on the specific material and desired chip evacuation characteristics. Ultimately, selecting the right PCD Reamer for Precision Holes is a critical investment in process stability, part quality, and overall cost efficiency.
The performance of a Wear-resistant PCD Reamer is defined by a set of precise technical parameters. Understanding these specifications is crucial for selecting the correct tool for your machining operation and ensuring optimal results. Key parameters include reamer diameter, flute design, cutting edge geometry, and shank type. Below is a detailed breakdown of standard and customizable specifications for our Wear-resistant PCD Reamer product line.
Product Specifications at a Glance:
- Material: High-grade PCD tips brazed onto a premium carbide or steel body.
- Primary Application: Finishing and semi-finishing of holes in abrasive non-ferrous materials (e.g., Aluminum, Silicon Aluminum, Composites, Copper Alloys).
- Key Benefit: Up to 100x longer tool life compared to carbide in abrasive applications.
- Surface Finish: Capable of achieving Ra ≤ 0.2 µm under optimal conditions.
- Tolerance Range: Standard offerings from h5 to h7, with tighter tolerances available upon request.
| Parameter | Standard Range / Description | Notes |
|---|---|---|
| Diameter Range (D) | 3.0 mm – 32.0 mm | Standard increments available; custom diameters possible. |
| Flute Type | Straight Flute, Spiral Flute (Right-hand) | Straight for general purpose; Spiral for improved chip evacuation in deep holes. |
| Number of Flutes | 4, 6, or 8 | More flutes enhance finish and stability; fewer flutes provide larger chip space. |
| Helix Angle (Spiral) | 15° or 30° | Higher angle for more aggressive chip removal in gummy materials. |
| Overall Length (L) | Varied based on diameter and application | Designed for sufficient reach and rigidity. |
| Shank Type | Straight Shank, Weldon Flat Shank | Compatible with standard CNC tool holders and collets. |
| Cutting Edge Geometry | Positive rake, polished cutting edge | Optimized for free-cutting action and minimal built-up edge. |
| Coolant Supply | Through-tool coolant channels (Optional) | Highly recommended for deep-hole reaming and effective chip flushing. |
Recommended Operating Parameters (Guide):
| Material | Cutting Speed (Vc) m/min | Feed Rate (f) mm/rev | Notes |
|---|---|---|---|
| Aluminum Alloys (e.g., AlSi) | 100 – 250 | 0.02 – 0.15 | Use higher speeds for finishing; adjust feed based on required finish and hole size. |
| Carbon Fiber Reinforced Plastic (CFRP) | 80 – 150 | 0.01 – 0.08 | Sharp edge and positive rake are critical to minimize delamination. |
| Copper & Brass | 60 – 120 | 0.03 – 0.10 | Polished flutes help prevent material adhesion. |
Related Products




Hot Products

CNC Prototype Model of Motor Housing
CNC Prototype Model of Motor Housing is a core precision product developed through years of practical manufacturing experience. Produced by Ningbo Wangdefu Precision Machinery, a trusted China manufacturer and factory, it is suitable for a wide range of new energy vehicle motors. With full-process capabilities from R&D to production, we deliver high-precision and reliable solutions. Our products have been supplied to leading automotive brands such as Volvo and NIO, earning strong recognition for quality and consistency.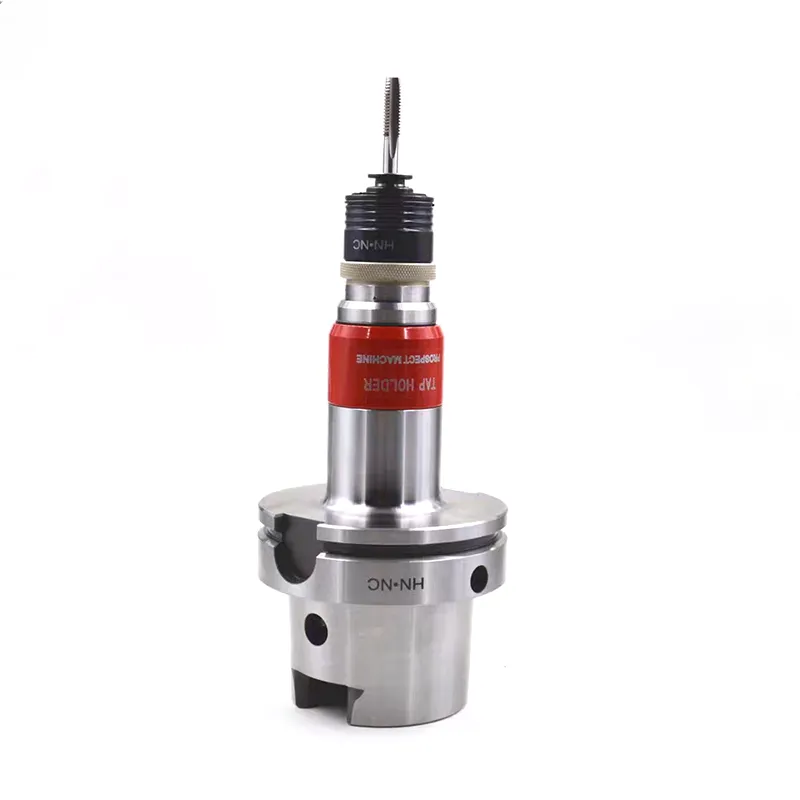
CNC Tapping Tool Handle
Looking for a reliable CNC tapping tool handle from a professional China manufacturer and supplier? Wangdefu provides high-precision CNC tapping tool systems that integrate threading tap holders, floating collets, and torque overload protection for safe, accurate, and efficient threading. Designed for automotive, mold-making, 3C electronics, and precision machinery industries, our solutions reduce tap breakage, improve thread quality, and enhance production efficiency. As a trusted factory and brand, Wangdefu ensures you get the best results with every project.
Spiral Flute Reamer
Spiral Flute Reamers from WDF are produced by a high-tech China manufacturer specializing in R&D, production, and sales. With over a decade of experience in precision tooling, our factory-level capabilities allow us to deliver customized solutions that enable faster, more accurate holemaking. Trusted by customers in automotive, aerospace, and precision machinery industries, WDF is a reliable supplier for high-quality, efficient machining tools.
PCD Corn End Mill
PCD Corn End Mills from Wangdefu are not just standard catalogue tools, but mature solutions repeatedly tested and optimized through long-term processing of aluminum alloys, new energy motor shells, and structural parts in our own China factory. As a professional manufacturer and supplier, Wangdefu delivers reliable, high-performance tools for mass production, with real expertise in landing practical machining solutions.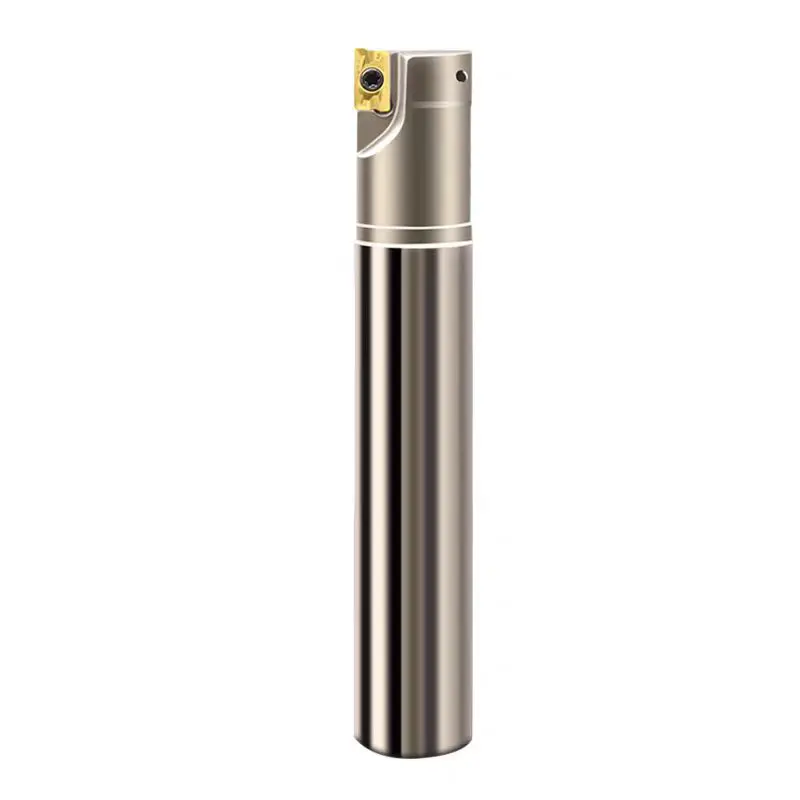
Square Shoulder End Mill
Square Shoulder End Mills from Wangdefu deliver stable, efficient, and durable solutions for high-precision machining of aluminum alloys, steel, stainless steel, and composites. As a professional China manufacturer and supplier, we provide customized tools and full-process technical support, ensuring one-time molding, high efficiency, and excellent machining accuracy for mass production.
CNC Prototype Valve Body
CNC Prototype Valve Body from Ningbo Wangdefu Precision Machinery is more than a precision component—it plays a critical role in vehicle active safety systems. As a trusted China manufacturer and factory, we bring over a decade of proven experience supplying precision parts for leading automotive brands. Market-validated and performance-driven, this valve body is engineered for customers who demand the highest standards of safety, reliability, and machining accuracy.
- Related Blog
- Reviews

