
PCD Reamer for Precision Holes
For manufacturing operations demanding ultimate accuracy and surface finish in non-ferrous and abrasive composite materials, the PCD Reamer stands as the definitive solution. Crafted from Polycrystalline Diamond, the hardest cutting tool material commercially available, this tool delivers exceptional performance where traditional carbide or high-speed steel reamers rapidly degrade. Its primary advantage lies in achieving and maintaining tight tolerances and micron-level surface finishes over exceptionally long production runs. This makes it the go-to tool for high-volume, precision-dependent industries such as aerospace, automotive engine manufacturing, and electronics.
Our Wear-resistant PCD Reamer is engineered to withstand the abrasive wear encountered in materials like carbon fiber composites, silicon-aluminum alloys, and green ceramics, dramatically reducing tool change frequency and machine downtime. For optimal chip evacuation in through-hole applications, our Straight Flute PCD Reamer offers superior performance. When processing blind holes or interrupted cuts, the Spiral Flute PCD Reamer provides smoother cutting action and improved finish. Regardless of the flute geometry, every tool in our lineup is a High-precision PCD Reamer, manufactured under stringent quality controls to ensure consistent, reliable results that meet the most demanding specifications.
The <产品名字> is built upon a robust carbide body, onto which a precisely lapped PCD cutting edge is brazed. This construction combines the extreme hardness and wear resistance of diamond with the structural integrity of carbide. The PCD tip is meticulously ground and polished to achieve a cutting edge with near-zero runout and a razor-sharp finish, which is critical for producing holes with minimal burnishing, no tearing, and a true cylindrical form. Its exceptional thermal conductivity also helps dissipate heat from the cutting zone, further protecting the workpiece material from thermal damage and preserving the metallurgical properties of aerospace-grade alloys.
Below are the detailed technical specifications and standard parameter options for our PCD Reamers. These configurations are designed to cover a wide range of standard and specialized applications.
- Body Material: Micro-grain carbide substrate for maximum rigidity.
- Cutting Edge Material: High-grade Polycrystalline Diamond (PCD) blank.
- Primary Applications: Non-ferrous metals (Aluminum, Copper, Brass), Abrasive Composites (CFRP, GFRP, MMC), Sintered Metals, and Ceramics.
- Standard Coating: Uncoated (PCD edge), with optional AlTiN coating on the carbide body for non-cutting surfaces.
- Quality Standard: 100% inspected for critical dimensions, cutting edge sharpness, and concentricity.
| Diameter (mm) | Flute Length (mm) | Overall Length (mm) | Shank Type | Flute Type | Tolerance (h6) |
|---|---|---|---|---|---|
| 3.00 - 6.00 | 10 - 20 | 60 - 80 | Straight Shank | Straight / Spiral | ±0.004 |
| 6.01 - 12.00 | 20 - 40 | 80 - 100 | Straight Shank | Straight / Spiral | ±0.005 |
| 12.01 - 20.00 | 30 - 50 | 100 - 120 | Straight Shank / Weldon | Straight / Spiral | ±0.006 |
| 20.01 - 30.00 | 40 - 70 | 120 - 150 | Weldon Shank | Spiral | ±0.008 |
For optimal performance, we recommend using our reamers with a high-pressure coolant system to ensure efficient chip removal. Machining parameters such as speed and feed should be adjusted based on the specific workpiece material, with typical cutting speeds ranging from 150 to 300 m/min for aluminum alloys. A proper, concentric setup with minimal tool overhang is crucial to achieve the stated tolerances and tool life.
Related Products




Hot Products

PCD Inserts
WDF is a professional China supplier specializing in PCD inserts. With many years of experience in the super-hard tooling industry, we have set an industry benchmark through advanced research and a precise understanding of customer needs. As a reliable manufacturer and factory-level provider, WDF has become a trusted partner for companies worldwide, delivering high-quality, precise, and durable cutting solutions.
Flat End Mill
WDF specializes in Flat End Mills, with long-term expertise in precision tool manufacturing and application. Ningbo Wangdefu Precision Machinery Co., Ltd. is supported by an experienced technical and service team and implements strict quality control throughout the production process to ensure stable performance and high accuracy. Our milling cutters deliver excellent precision and surface finish, helping automotive parts manufacturers complete complex and high-end machining tasks efficiently. As a reliable China manufacturer, we are committed to building long-term partnerships with global customers.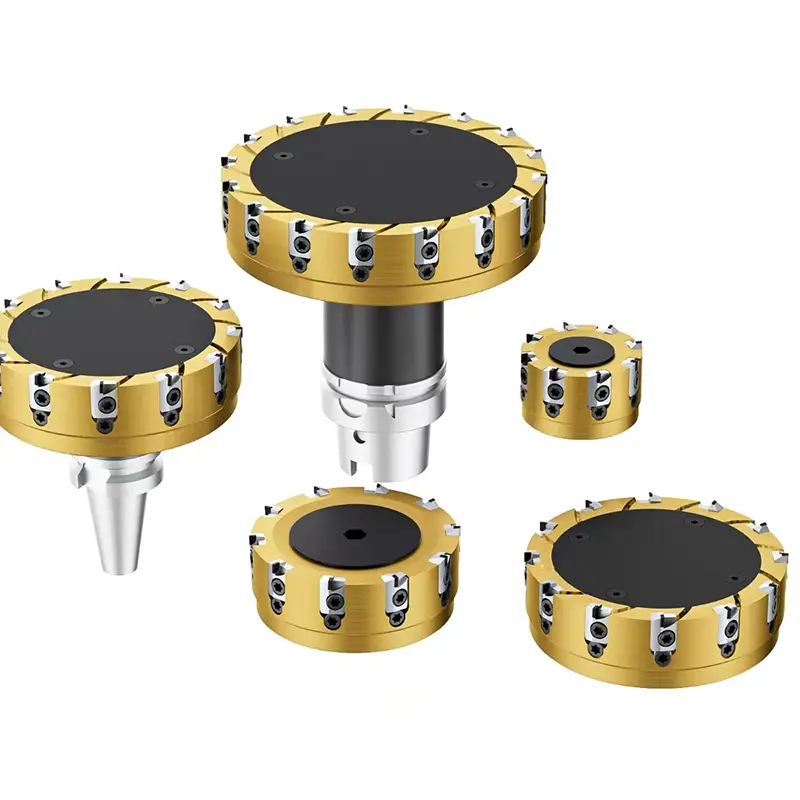
Aluminum Alloy Face Milling Cutter Tool
The Aluminum Alloy Face Milling Cutter Tool from Ningbo Wangdefu Precision Machinery Co., Ltd is designed for high-efficiency, high-precision machining of aluminum and aluminum alloy materials. Backed by years of manufacturing experience and strict factory-level quality control, each cutter delivers stable performance, excellent surface finish, and long tool life for demanding industrial applications.
As a professional China aluminum milling cutter manufacturer and supplier, Wangdefu controls every stage of production—from raw material selection to final inspection—to ensure consistent accuracy and reliable machining results. Our face milling cutters are widely used in automotive parts, aerospace components, and precision mechanical manufacturing.
CNC Tapping Tool Handle
Looking for a reliable CNC tapping tool handle from a professional China manufacturer and supplier? Wangdefu provides high-precision CNC tapping tool systems that integrate threading tap holders, floating collets, and torque overload protection for safe, accurate, and efficient threading. Designed for automotive, mold-making, 3C electronics, and precision machinery industries, our solutions reduce tap breakage, improve thread quality, and enhance production efficiency. As a trusted factory and brand, Wangdefu ensures you get the best results with every project.
Carbide Straight Flute Tap
Looking for a high-performance Carbide straight flute tap from a reliable China manufacturer? At Wangdefu, we specialize in precision cutting tools that deliver long-life, consistent performance, and superior thread accuracy. As a trusted supplier and factory, we serve automotive, aerospace, mold-making, and precision machinery industries worldwide. Our taps help you reduce production costs, improve efficiency, and achieve high-quality thread machining results, making Wangdefu your go-to brand for precision straight flute taps.
CNC Milling Non-Standard Cutter Head
In the fields of precision machining and high-end manufacturing, efficiency, accuracy, and tool compatibility are the most important concerns for buyers. As a leading supplier in China, Wangdefu focuses on providing high-performance CNC milling non-standard cutter heads to meet the machining needs of various complex parts.
- Related Blog
- Reviews

