
PCD Insert for Copper Alloy
PCD Inserts for Copper Alloy Machining
Machining copper alloys presents a unique set of challenges, demanding tools that can handle high thermal conductivity, prevent material adhesion, and deliver a superior surface finish. Our precisely engineered PCD (Polycrystalline Diamond) inserts are the definitive solution. Unlike conventional carbide tools, our Application-Specific PCD Insert is designed from the ground up to address the specific demands of copper and its alloys such as brass and bronze. The exceptional hardness and wear resistance of synthetic diamond ensure unparalleled tool life, reducing downtime and operational costs. For intricate profiles and finishing operations, our PCD Diamond-Shaped Insert geometry offers precision and stability. As a premier Wear-Resistant PCD Insert, it maintains a sharp cutting edge far longer than any other material, guaranteeing consistent part quality over extended production runs. This makes it an indispensable PCD Insert for Non-Ferrous Metals, excelling in high-speed, high-volume applications where surface integrity and dimensional accuracy are non-negotiable.
The PCD Insert for Copper Alloy is manufactured using premium synthetic diamond particles sintered under high pressure and temperature onto a robust tungsten carbide substrate. This process creates a tool with a perfect synergy of extreme hardness and exceptional toughness. The ultra-smooth PCD surface minimizes friction and virtually eliminates built-up edge (BUE), a common issue when machining gummy materials like copper. This results in significantly improved chip flow, reduced cutting forces, and a mirror-like surface finish on the workpiece. The substrate provides the necessary strength to withstand cutting pressures and intermittent cuts, ensuring reliable performance in various machining operations from turning and milling to boring. Optimized rake angles and edge preparations are applied to our PCD Insert for Copper Alloy to further enhance shearing action and reduce power consumption.
Key Specifications & Advantages
- Material: Premium Polycrystalline Diamond (PCD) layer on Tungsten Carbide substrate.
- Primary Application: High-speed finishing and semi-finishing of copper, brass, bronze, and other non-ferrous alloys.
- Exceptional Wear Resistance: Tool life can be 50 to 100 times longer than carbide in copper alloy machining.
- Superior Surface Finish: Produces excellent surface quality, often eliminating secondary polishing operations.
- High Thermal Conductivity: Effectively dissipates heat from the cutting zone, protecting the workpiece material.
- Anti-Adhesion Properties: Smooth PCD surface prevents material welding and built-up edge formation.
Standard Grades & Geometries
| PCD Grade | Grain Size (µm) | Recommended Operation | Typical Geometry |
|---|---|---|---|
| Fine Grain | 2-10 | Mirror finishing, high-precision boring | Sharp edge, positive rake |
| Medium Grain | 10-25 | General turning, face milling, semi-finishing | Chamfered edge, versatile rake |
| Coarse Grain | 25-50 | Heavy roughing, interrupted cuts | Honed edge, strong negative rake |
Performance Data Summary
| Workpiece Material | Cutting Speed (m/min) | Feed Rate (mm/rev) | Depth of Cut (mm) | Expected Tool Life Improvement* |
|---|---|---|---|---|
| Copper (C11000) | 300 - 800 | 0.10 - 0.30 | 0.5 - 3.0 | Up to 100x |
| Free-Cutting Brass (C36000) | 400 - 1000 | 0.15 - 0.40 | 1.0 - 4.0 | 50x - 80x |
| Aluminum Bronze (C95400) | 150 - 400 | 0.08 - 0.25 | 0.5 - 2.5 | 30x - 60x |
*Compared to uncoated carbide tools under similar conditions.
Related Products




Hot Products
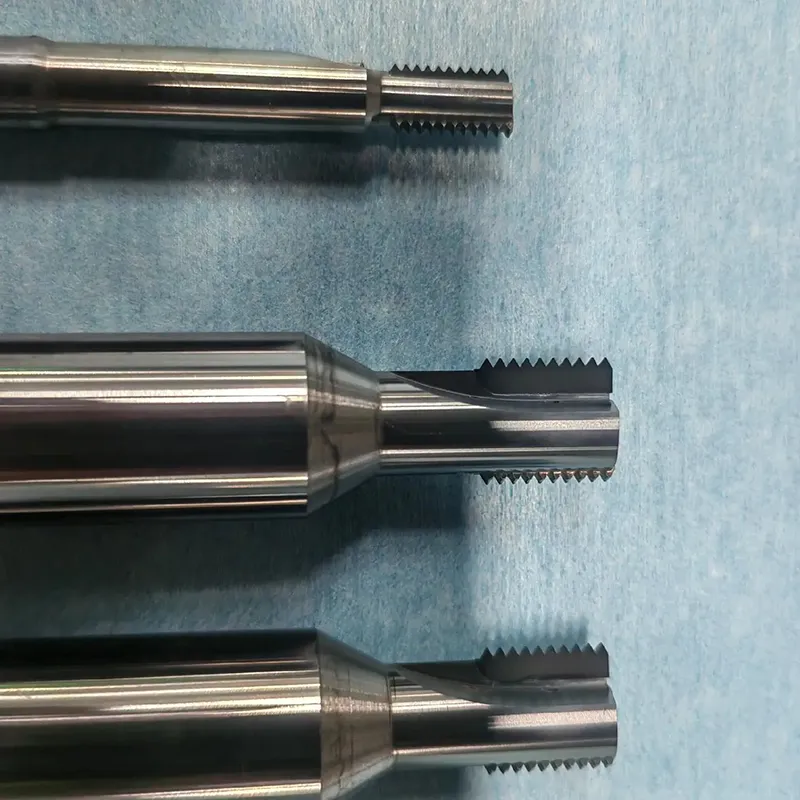
UNF-metric Thread Drilling and Threading Cutter
Looking for a reliable UNF-metric thread drilling and threading cutter manufacturer in China? At Wangdefu, we provide high-precision, long-life UNF cutters suitable for automotive, aerospace, and precision machinery applications. As a trusted supplier and factory, we deliver fast, high-quality solutions to help you reduce production costs and improve efficiency. Our cutters ensure thread accuracy, stable performance, and consistent results across batches, making us your ideal partner for high-precision UNF thread machining.
Shrink Fit Chuck
WDF is a high-tech China manufacturer specializing in the research, development, and production of shrink fit chucks. With years of experience in the precision tooling industry, we provide customized solutions focused on high rigidity, low vibration, and quick-change efficiency. Using advanced equipment and factory-level quality control, WDF ensures exceptional performance in high-end manufacturing, earning a strong reputation as a reliable supplier worldwide.
Runout Adjustable Flange Adapter
As a leading China manufacturer and supplier, Wangdefu proudly presents the Runout Adjustable Flange Adapter, a high-end precision tool holder designed for demanding CNC machining applications. From automotive parts to aerospace components, our flange adapter allows manufacturers, engineers, and factories to achieve micron-level accuracy, high rigidity, and ultra-stable performance. With Wangdefu’s expertise in precision CNC tools and decades of experience in the industry, our solution simplifies supply chains, improves production efficiency, and reduces machining errors, making it the preferred choice for professional workshops and factories worldwide.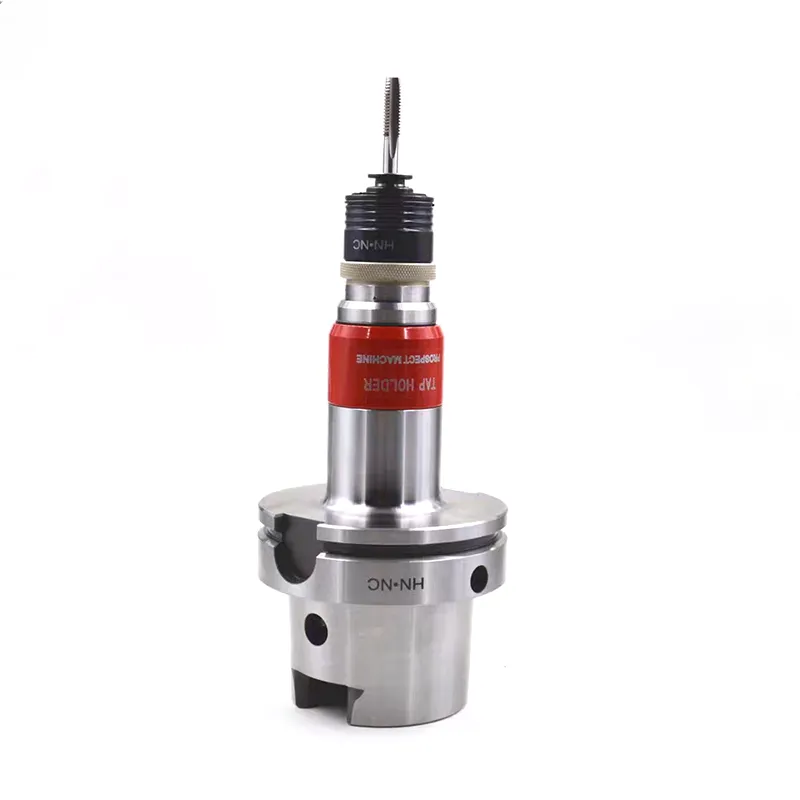
CNC Tapping Tool Handle
Looking for a reliable CNC tapping tool handle from a professional China manufacturer and supplier? Wangdefu provides high-precision CNC tapping tool systems that integrate threading tap holders, floating collets, and torque overload protection for safe, accurate, and efficient threading. Designed for automotive, mold-making, 3C electronics, and precision machinery industries, our solutions reduce tap breakage, improve thread quality, and enhance production efficiency. As a trusted factory and brand, Wangdefu ensures you get the best results with every project.
Carbide Twist Drill Bits
WDF specializes in drilling tools. Our Carbide Twist Drill Bits are made from top-quality, hardened carbide! They're incredibly tough, incredibly durable, and incredibly durable, making them perfect for high-speed cutting. They produce precise, smooth holes, work incredibly quickly, and eliminate the need for subsequent repairs. Their unique design makes them easy to drill even high-hardness metals and difficult-to-cut materials. They're used in industries like machine tools, automotive parts, and aerospace—the perfect choice for demanding work!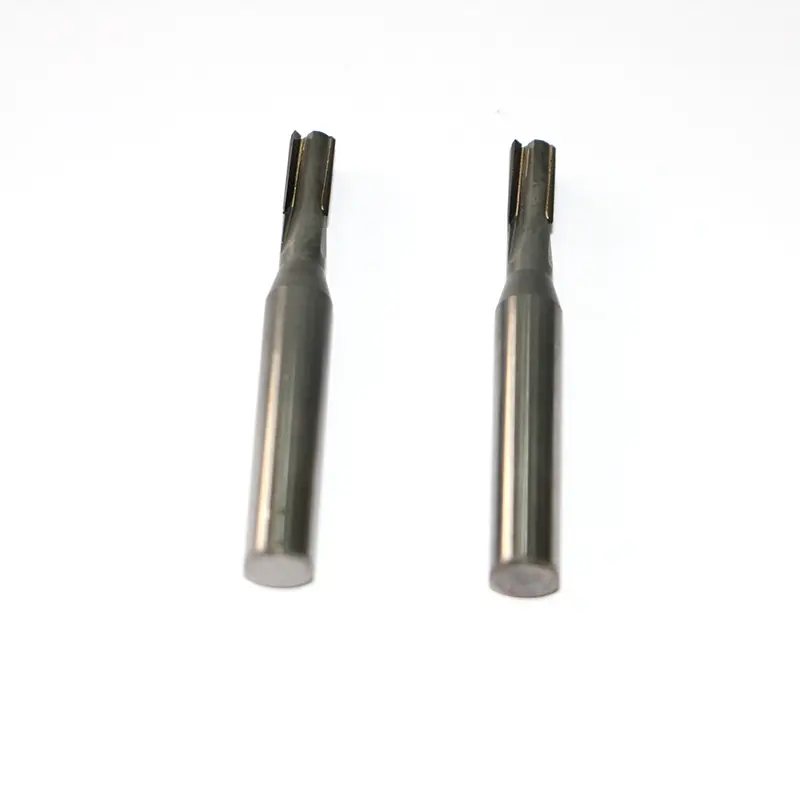
PCD End Mill
As a China PCD tool manufacturer with more than ten years of deep precision manufacturing, Wangdefu focuses on providing high-performance PCD End Mill solutions for automotive parts, new energy motor housings and robot core structural parts.
We do not just sell tools, but from material analysis, tool structure design, parameter matching to mass production verification, to help customers truly solve the problems of low machining efficiency, short tool life, unstable surface quality, etc.
- Related Blog
- Reviews

