
Face Mill With Interchangeable Inserts
For machining professionals seeking exceptional surface finish and high metal removal rates, a Face Mill for Machining Center equipped with interchangeable inserts is a cornerstone tool. Our High-Precision Face Mill series is engineered for stability and accuracy, delivering consistent results in demanding applications. Specifically, when working with non-ferrous materials, our dedicated PCD Aluminum Face Mill and PCD Face Mill For Aluminum Processing utilize advanced Polycrystalline Diamond (PCD) inserts to achieve mirror-like finishes on aluminum alloys while dramatically extending tool life and minimizing built-up edge.
The core advantage of our <产品名字> lies in its versatile design and robust construction. It allows for quick and easy insert changes, minimizing machine downtime and providing cost efficiency through the use of standard, readily available indexable inserts. The precision-ground body ensures perfect insert seating, which is critical for maintaining tight tolerances and achieving superior surface quality across the entire workpiece. This tool is indispensable for face milling, shoulder milling, and slab milling operations across various industries. Below are the detailed specifications that define its performance envelope.
Key Features & Benefits
- Modular Insert System: Enables rapid changeover between different insert grades (e.g., carbide, ceramic, PCD) for diverse materials and operations.
- Optimized Geometry: Designed for high-efficiency chip evacuation, reducing heat buildup and preventing re-cutting of chips.
- High Rigidity Body: Manufactured from premium steel with precise balancing for vibration-free operation at high speeds and feeds.
- Axial and Radial Adjustability: Some models feature fine adjustment screws for exact insert positioning to compensate for wear and ensure flawless flatness.
- Wide Range of Sizes: Available in multiple diameters to suit different machine capacities and part dimensions.
Technical Specifications
| Parameter | Specification / Range | Notes |
|---|---|---|
| Body Diameter (D) | 50 mm - 250 mm (2" - 10") | Custom sizes available upon request. |
| Cutting Diameter (DC) | 55 mm - 260 mm | Varies with insert size and mounting. |
| Number of Inserts | 5, 6, 8, 10, 12 | Depends on cutter diameter and pitch. |
| Insert Shape / Type | Square (SNMM/SNMG), Round (RPMT), Octagon | Compatible with industry-standard ISO inserts. |
| Shank Type | CAT/BT 40, 50; HSK 63, 100; Straight Shank | To match common machining center spindles. |
| Axial Rake Angle | 15° (Positive) | Promotes free cutting and reduces power consumption. |
| Recommended Radial DOC (ap) | 0.5 - 6.0 mm | Varies based on material, insert grade, and machine power. |
| Recommended Axial DOC (ae) | Up to 75% of DC | For optimal surface finish and tool engagement. |
| Max. Spindle Speed (RPM) | 6,000 - 15,000+ | Dependent on balance grade (G2.5/G6.3) and diameter. |
| Coolant Supply | Through-tool coolant channels (Optional) | Enhances chip evacuation and cooling at the cutting edge. |
Cutting Data Guidelines (For Steel & Aluminum)
| Workpiece Material | Insert Grade | Cutting Speed Vc (m/min) | Feed per Tooth fz (mm) | Application Note |
|---|---|---|---|---|
| Mild Steel (AISI 1045) | Carbide, PVD Coated | 180 - 280 | 0.10 - 0.25 | Use emulsion coolant for best results. |
| Stainless Steel (AISI 304) | Carbide, Milling Specific | 80 - 120 | 0.08 - 0.18 | Ensure rigid setup to combat work hardening. |
| Aluminum Alloy (6061) | Uncoated Carbide or PCD | 500 - 2500+ | 0.10 - 0.40 | PCD inserts recommended for high-volume, finish-critical work. |
| Cast Iron (Gray) | Carbide, CVD Coated | 70 - 120 | 0.12 - 0.30 | Dry cutting or with air blast is often suitable. |
Related Products


Hot Products

Forming Milling Cutter
Forming Milling Cutters from WDF are produced with full-service support from design to manufacturing. As a leading China manufacturer and factory, we combine years of experience with dozens of high-precision machines to ensure each cutter meets exacting standards. Trusted supplier in the industry, WDF delivers reliable, high-quality tools for demanding machining applications.
Carbide Thread Cutting Taps
Looking for a reliable China Manufacturer for high-precision Carbide Thread Cutting Taps? At Wangdefu, we specialize in premium carbide taps for carbon steel, stainless steel, mold steel, cast iron, and more. Our taps achieve 6H–7H thread tolerance, support through-hole and blind-hole threading, and ensure high efficiency, long tool life, and low breakage. Trusted by automotive, mold, and precision machinery manufacturers worldwide, we deliver consistent results and optimized production.
End Mill Bits
End Mill Bits from WDF are produced with advanced equipment and decades of industry experience. As a trusted China manufacturer and supplier with factory-level production, every milling cutter is meticulously crafted and inspected for precision. Highly praised by domestic and international customers, WDF delivers reliable, high-quality tools for demanding machining applications.
Triple-Flute Internal Cooling Carbide Drill Bit
Wangdefu is a leading CNC tool manufacturer and factory in China. We focus on the R & D and production of high precision CNC tools. Our Triple-flute internal cooling carbide drill bit combines a triple-helix fluted design with internal cooling channels to provide superior performance in high-speed, high-precision machining. This tool is especially suitable for the automotive, robotics, aerospace and mold manufacturing industries, significantly improving machining efficiency and hole location accuracy, reducing tool wear and production risks.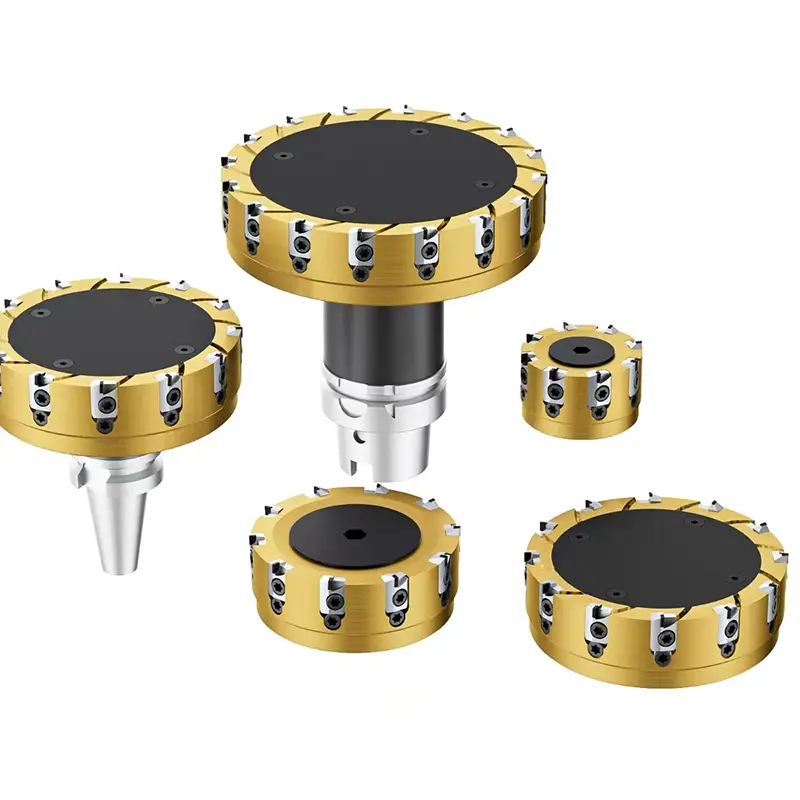
Aluminum Alloy Face Milling Cutter Tool
The Aluminum Alloy Face Milling Cutter Tool from Ningbo Wangdefu Precision Machinery Co., Ltd is designed for high-efficiency, high-precision machining of aluminum and aluminum alloy materials. Backed by years of manufacturing experience and strict factory-level quality control, each cutter delivers stable performance, excellent surface finish, and long tool life for demanding industrial applications.
As a professional China aluminum milling cutter manufacturer and supplier, Wangdefu controls every stage of production—from raw material selection to final inspection—to ensure consistent accuracy and reliable machining results. Our face milling cutters are widely used in automotive parts, aerospace components, and precision mechanical manufacturing.
Hydraulic Tool Holder
Looking for a reliable Hydraulic Tool Holder manufacturer in China? Wangdefu Precision Machinery, a trusted supplier and factory with over a decade of experience in CNC tooling and prototype solutions, offers high-precision, durable, and high-speed clamping systems. Our hydraulic tool holders are designed for aerospace, precision mold, 3C electronics, and medical device applications, providing micrometer-level accuracy, ultra-high rigidity, and repeatable performance. Whether you are sourcing for milling, drilling, or high-speed cutting operations, Wangdefu delivers professional solutions tailored to your production needs.
- Related Blog
- Reviews

